


Why is your drill always unstable?
Defining the quality of hole machining is actually difficult because
If the hole has strict tolerance or surface finish requirements, secondary machining such as boring or reaming usually completes the hole to the final machining size. In these cases, the main value of a drill bit may be to drill as many holes as possible as quickly, and what users can see is whether the positioning is accurate.
But this is not always the case. In some applications, spending more time and effort may help the drill bit meet quality standards in one operation. Alternatively, it can be determined that the quality of the drilling affects its ability to accept high-quality secondary processing. For example, if drilling at an excessively high speed, heat may cause the material to work hard, greatly reducing the lifespan of the tap and even making the material too hard to be tapped.
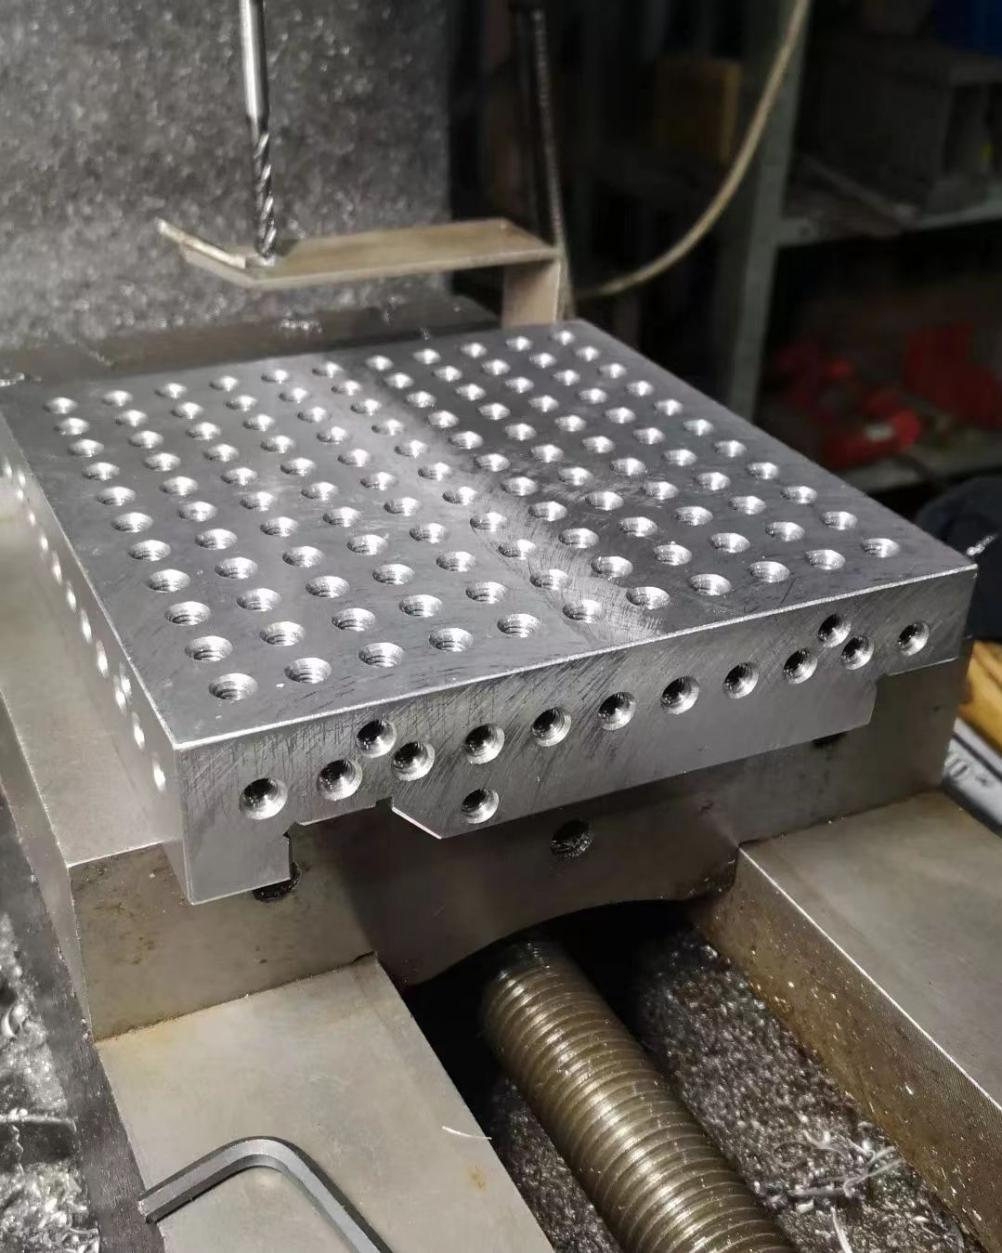
If a hard alloy drill bit drills 2 or 200 holes, it may be different; If it is 200, the quality focus may mainly be on the speed (efficiency) of completing the work; If this job only requires 2 holes, spending more time and effort during the drilling process, or using specially designed tools to drill and ream holes in one operation, can produce holes that meet quality specifications without additional processes.
Maybe there are three questions that come to my mind here
Does it meet the tolerance of the hole.
Does 2 meet the requirements for hole machining.
Whether the concentricity is good.
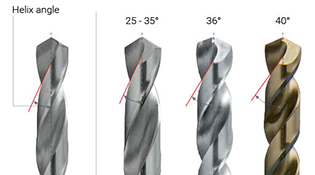
Hard alloy drill bits are actually applied in many fields, but many technologies are also overlooked. The design of spiral angles is also very particular, such as low spiral angles or straight groove drill bits, which are very suitable for short chip materials such as cast iron and ductile iron. For example, a spiral angle of 20-30 ° is conducive to universal drilling in various hard materials, as this angle helps to remove chips.
However, aluminum and copper tend to have high helix angles, which provide a predictive effect and aid in chip removal. Choosing drill bits with the correct characteristics for specific materials and applications will prolong tool life and achieve good smoothness.
The coating also has significant differences. Usually, for example, some brands of drill bits will use composite coatings that can fully exert their effects, including titanium, chromium, and titanium silicon layers.
Silicon gives the coating high lubricity, so chips can slide off and avoid the formation of chip deposits. Avoiding chip buildup is the key to maintaining good cutting ability of the tool and avoiding leaving marks on the hole wall.
Some new coatings are combined with higher speeds to remove materials and produce pores with good smoothness. These coatings need to be able to withstand the heat generated by high-speed motion.
one
Control the details of the drill bit
Choosing the appropriate bar material, the quality of the hole has already started from the process design. If the runout is too large, it will sacrifice the accuracy, smoothness, and concentricity of the hole. The appropriate core thickness on the drill tip is important for the drill bit to maintain stability when joining with the processed material, in order to prevent the drill bit from being too large and offset, which can cause the hole to be too large or affect the straightness of the hole.
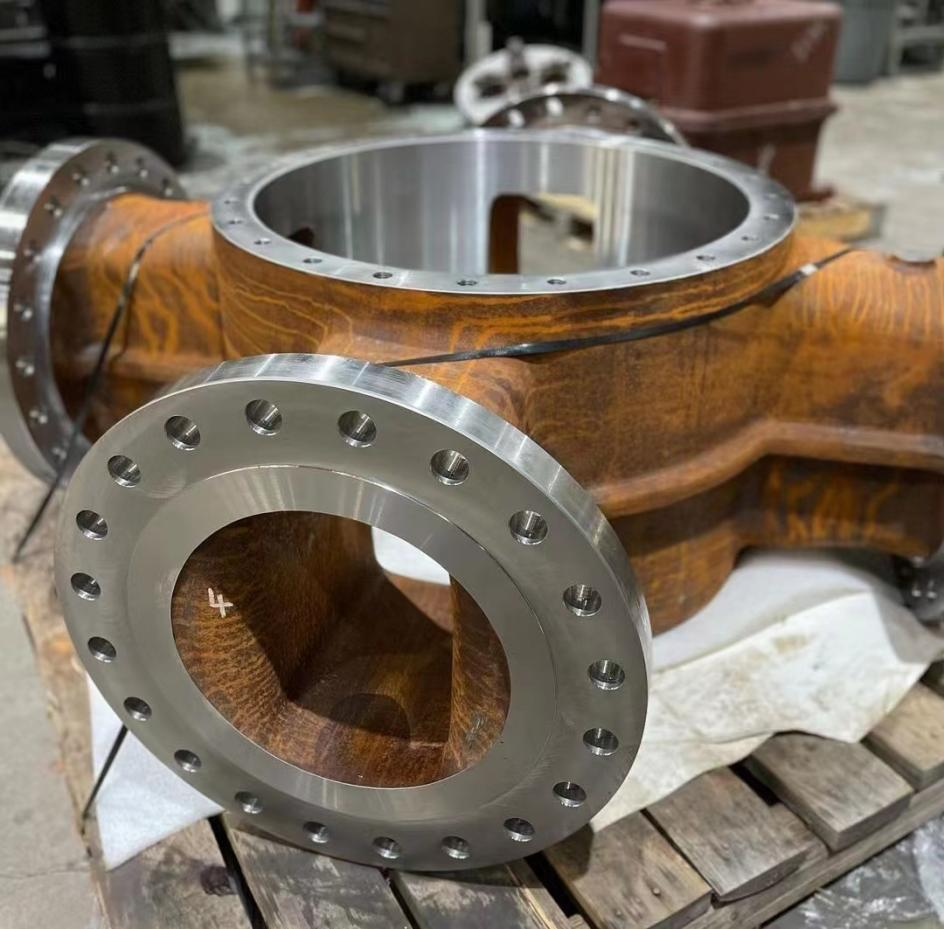
When quality requirements include improving tolerances and surface finish, changing from single ligament to double ligament on drill bits can be helpful.
These edges stabilize the drill bit by providing four contact points in the hole and provide a polishing effect to leave a very good finish. The double ligaments also serve as a guide, keeping the drill bit moving forward in a straight line, especially in deep holes. It can prevent the drill bit from getting bigger and shaking, thereby providing a relatively round hole.
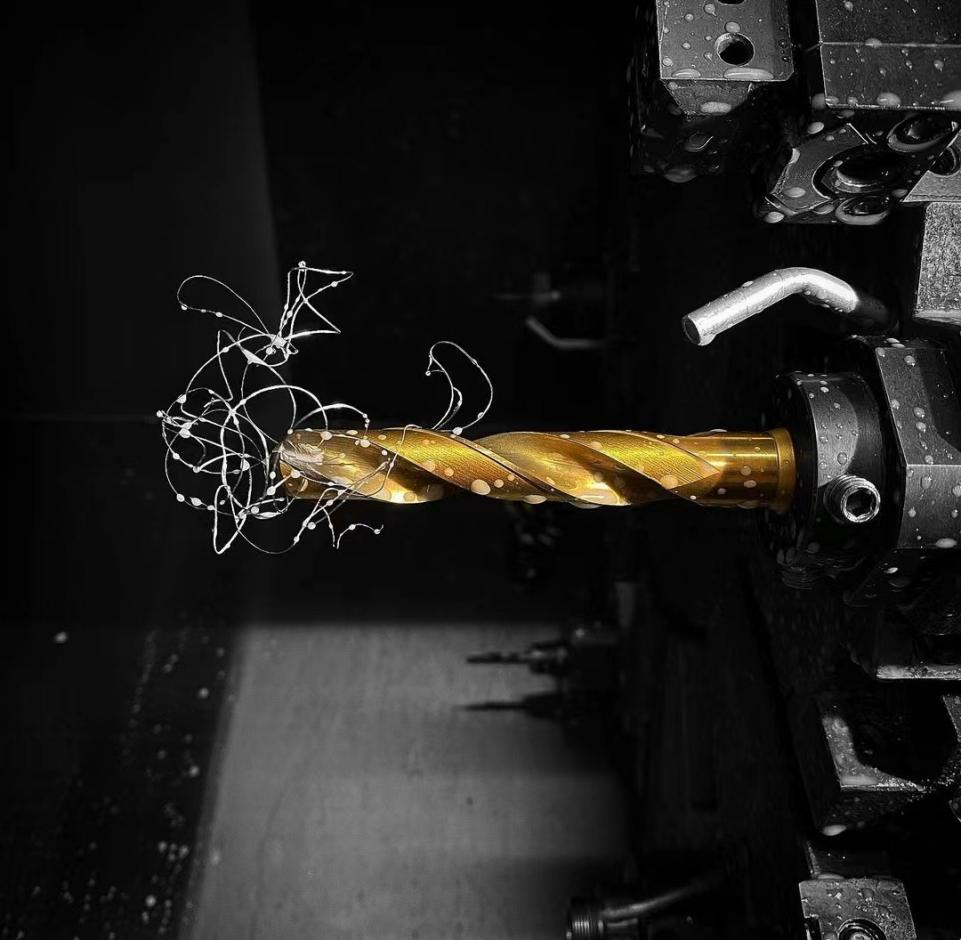
Although double ligament drills produce good surfaces in short chip materials, it is recommended to use single ligament drills when the material produces growing chips. For long chip materials like aluminum or stainless steel, single ligament drills are the preferred choice. The use of double ligament stainless steel drill bits can cause chips to enter the contact point between the drill bit and the material.
Controlling jumping is another key aspect of hole quality. Jumping too much can cause the processed aperture to become larger, and as the drill bit speed increases and rotates, it will cause the drill bit to drill larger and larger holes.
A drill bit that is too long can lead to poor rigidity and generate vibration. These vibrations, especially those that are difficult to see with a small drill bit, can cause the drill bit to break and leave a broken blade on the inner hole surface.
two
Control of cutting fluid
Proper coolant management, including maintaining optimal coolant concentration, filtration, and pressure, is crucial in drilling applications.
The appropriate concentration of coolant increases lubrication while taking away the heat from the cutting edge of the drill bit. Filtering can remove metal pollutants and other substances, thereby improving drilling performance and preventing problems such as coolant hole blockage in small diameter drill bits.
Preventing chips from entering the wall between the drill bit and the material being processed is crucial for the quality of the hole. The shape and color of these chips can help operators determine whether the quality of the holes drilled by the drill bit is good or bad.
It is important for the chip removal groove of the drill bit to produce beautiful conical chips. Two to three curled or braided chips may entangle in the chip chute and rub and scratch both sides of the hole. This friction can cause surface roughness.
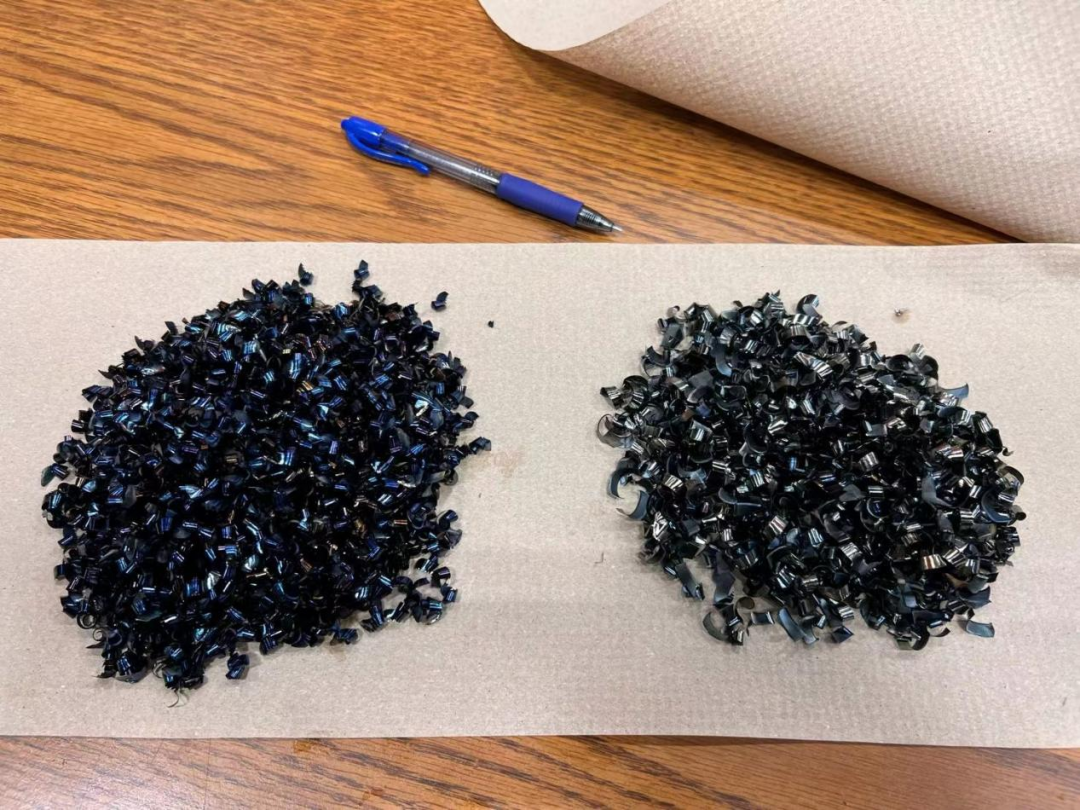
The back of the chip should be silver and shiny. Unlike when milling, you want to see blue (this picture only shows the color of the chips, not the drilling chips), because this means that heat enters the chips, and blue represents that your hole machining means generating a large amount of heat on the cutting edge. This heat will cause the blade to wear out faster.
Many times, when measuring the quality of a cutting tool, stability is a core indicator, which is also the difference between large and small factories. Therefore, it is recommended that factory owners not be fooled by temporary low prices, as the time cost invested by everyone is still high. It is best to find professional manufacturers as much as possible.


