Types, performance, characteristics, and application expertise of 6 types of CNC cutting tools
The combination of advanced processing equipment and high-performance CNC cutting tools is necessary to fully exert its due efficiency and achieve good economic benefits. With the rapid development of tool materials, various new types of tool materials have greatly improved their physical, mechanical, and cutting performance, and their application scope is also constantly expanding.
1 The tool material should have basic properties
The selection of tool materials has a significant impact on tool life, processing efficiency, processing quality, and processing costs. Cutting tools must withstand high pressure, high temperature, friction, impact, and vibration during cutting. Therefore, tool materials should have the following basic properties:
(1) Hardness and wear resistance. The hardness of the tool material must be higher than that of the workpiece material, generally requiring a hardness of 60HRC or above. The higher the hardness of the tool material, the better its wear resistance.
(2) Strength and toughness. The tool material should have high strength and toughness to withstand cutting forces, impacts, and vibrations, and to prevent brittle fracture and edge collapse of the tool.
(3) Heat resistance. The tool material has good heat resistance, can withstand high cutting temperatures, and has good oxidation resistance.
(4) Process performance and economy. The tool material should have good forging performance, heat treatment performance, and welding performance; Grinding performance, and the pursuit of high cost performance ratio.
2, Types, properties, characteristics, and applications of cutting tool materials
1. Types, properties, characteristics, and tool applications of diamond cutting tool materials
Diamond is an allotrope of carbon, and it is the hardest material found in nature. Diamond cutting tools have high hardness, wear resistance, and thermal conductivity, and are widely used in the processing of non-ferrous and non-metallic materials. Especially in high-speed cutting of aluminum and silicon aluminum alloys, diamond cutting tools are the main type of cutting tools that are difficult to replace. Diamond cutting tools that can achieve high efficiency, high stability, and long service life are indispensable and important tools in modern CNC machining.
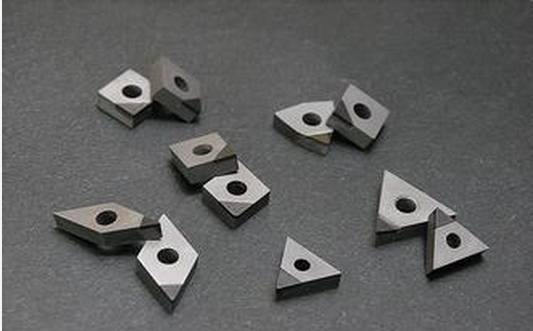
⑴ Types of diamond cutting tools
① Natural diamond cutting tools: Natural diamond has a history of over a hundred years as a cutting tool. After fine grinding, natural single crystal diamond cutting tools can have extremely sharp edges, with a cutting radius of up to 0.002 μ m. Being able to achieve ultra-thin cutting and achieve extremely high workpiece accuracy and low surface roughness, it is a recognized, ideal, and irreplaceable ultra precision machining tool.
② PCD diamond cutting tools: Natural diamond is expensive, and polycrystalline diamond (PCD) is still widely used in cutting processing. Since the early 1970s, After the successful development of polycrystalline diamond (PCD) blades prepared by high-temperature and high-pressure synthesis technology, natural diamond cutting tools have been replaced by artificial polycrystalline diamond in many situations. PCD raw materials are abundant, and their prices are only tens to tens of times that of natural diamond.
PCD tools cannot grind extremely sharp edges, and the surface quality of the processed workpiece is not as good as natural diamond. Currently, it is not convenient to manufacture PCD blades with chip grooves in industry. Therefore, PCD can only be used for precision cutting of non-ferrous metals and non-metals, making it difficult to achieve ultra precision mirror cutting.
③ CVD diamond cutting tools: Since the late 1970s to early 1980s, CVD diamond technology has emerged in Japan. CVD diamond refers to the synthesis of diamond films on heterogeneous substrates (such as hard alloys, ceramics, etc.) using chemical vapor deposition (CVD). CVD diamond has the same structure and characteristics as natural diamond.
The performance of CVD diamond is very similar to that of natural diamond, and it combines the advantages of natural single crystal diamond and polycrystalline diamond (PCD), which to some extent overcomes their shortcomings.
⑵ Performance characteristics of diamond cutting tools
① Extremely high hardness and wear resistance: Natural diamond is the hardest substance found in nature. Diamond has extremely high wear resistance. When processing high hardness materials, the lifespan of diamond cutting tools is 10-100 times that of hard alloy cutting tools, and even hundreds of times longer.
② Has a very low friction coefficient: The friction coefficient between diamond and some non-ferrous metals is lower than other cutting tools, with low friction coefficient and small deformation during machining, which can reduce cutting force.
③ The cutting edge is very sharp: the cutting edge of diamond tools can be ground very sharp, and natural single crystal diamond tools can reach as high as 0.002-0.008 μ m. Capable of ultra-thin cutting and ultra precision machining.
④ Has high thermal conductivity: Diamond has a high thermal conductivity and thermal diffusion rate, and cutting heat is easily dissipated. The cutting temperature of the tool is low.
⑤ Having a lower coefficient of thermal expansion: The thermal expansion coefficient of diamond is several times smaller than that of hard alloy, and the change in tool size caused by cutting heat is very small, which is particularly important for precision and ultra precision machining with high dimensional accuracy requirements.
Application of diamond cutting tools
Diamond cutting tools are commonly used for fine cutting and boring of non-ferrous and non-metallic materials at high speeds. Suitable for processing various wear-resistant non-metallic materials, such as fiberglass powder metallurgy blanks, ceramic materials, etc; Various wear-resistant non-ferrous metals, such as various silicon aluminum alloys; Various non-ferrous metal finishing processes.
The disadvantage of diamond cutting tools is their poor thermal stability. When the cutting temperature exceeds 700 ℃ to 800 ℃, their hardness will be completely lost; In addition, it is not suitable for cutting black metals because diamond (carbon) easily interacts with iron atoms at high temperatures, converting carbon atoms into graphite structures, making the tool extremely susceptible to damage.
2. Types, properties, characteristics, and tool applications of cubic boron nitride tool materials
The second superhard material, cubic boron nitride (CBN), synthesized using a method similar to diamond manufacturing, is second only to diamond in terms of hardness and thermal conductivity. It has excellent thermal stability and does not oxidize when heated to 10000C in the atmosphere. CBN has extremely stable chemical properties for black metals and can be widely used in the processing of steel products.
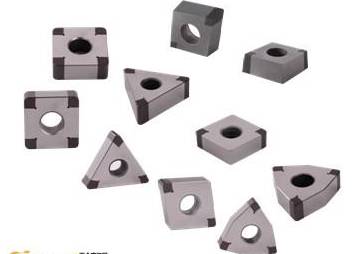
Types of cubic boron nitride cutting tools
Cubic boron nitride (CBN) is a substance that does not exist in nature and can be divided into single crystal and polycrystalline, namely CBN single crystal and polycrystalline cubic boron nitride (PCBN). CBN is one of the isomers of boron nitride (BN), with a structure similar to diamond.
PCBN (Polycrystalline Cubic Boron Nitride) is a polycrystalline material that sinters fine CBN materials together through binding phases (TiC, TiN, Al, Ti, etc.) under high temperature and pressure. It is currently the second hardest tool material synthesized artificially, and together with diamond, it is referred to as superhard tool material. PCBN is mainly used for making cutting tools or other tools.
PCBN cutting tools can be divided into integral PCBN blades and PCBN composite blades sintered with hard alloy composites.
PCBN composite blades are made by sintering a layer of O.5-1.0mm thick PCBN on a hard alloy with good strength and toughness. Its performance combines good toughness, high hardness, and wear resistance, solving the problems of low bending strength and welding difficulties of CBN blades.
The main properties and characteristics of cubic boron nitride
Although the hardness of cubic boron nitride is slightly lower than diamond, it is much higher than other high hardness materials. The outstanding advantage of CBN is that its thermal stability is much higher than that of diamond, reaching over 1200 ℃ (700-800 ℃ for diamond), and another outstanding advantage is its high chemical inertness, which does not react with iron elements at 1200-1300 ℃. The main performance characteristics of cubic boron nitride are as follows.
① High hardness and wear resistance: CBN crystal structure is similar to diamond, with similar hardness and strength to diamond. PCBN is particularly suitable for processing high hardness materials that could only be ground before, and can achieve better surface quality of workpieces.
② It has high thermal stability: the heat resistance of CBN can reach 1400-1500 ℃, which is almost 1 times higher than the heat resistance of diamond (700-800 ℃). PCBN tools can cut high-temperature alloys and quenched steel at a speed 3-5 times higher than hard alloy tools.
③ Excellent chemical stability: It does not react chemically with iron based materials even at temperatures between 1200-1300 ℃, and does not wear sharply like diamond. At this time, it can still maintain the hardness of hard alloys; PCBN cutting tools are suitable for cutting quenched steel parts and cold hard cast iron, and can be widely used for high-speed cutting of cast iron.
④ Having good thermal conductivity: Although the thermal conductivity of CBN cannot catch up with diamond, the thermal conductivity of PCBN is second only to diamond in various tool materials, much higher than that of high-speed steel and hard alloys.
⑤ Having a lower coefficient of friction: A lower coefficient of friction can lead to a decrease in cutting force, a decrease in cutting temperature, and an improvement in surface quality during machining.
Application of cubic boron nitride cutting tools
Cubic boron nitride is suitable for precision machining of various difficult to cut materials such as quenched steel, hard cast iron, high-temperature alloys, hard alloys, and surface spray materials. The machining accuracy can reach IT5 (hole IT6), and the surface roughness value can be as low as Ra1.25-0.20 μ M.
The toughness and bending strength of cubic boron nitride cutting tool materials are poor. Therefore, cubic boron nitride turning tools are not suitable for rough machining at low speeds and with high impact loads; It is not suitable for cutting materials with high plasticity, such as aluminum alloys, copper alloys, nickel based alloys, and steel with high plasticity, because cutting these metals will produce serious chip deposits, which will deteriorate the machining surface.
3. Types, properties, characteristics, and tool applications of ceramic tool materials
Ceramic cutting tools have the characteristics of high hardness, good wear resistance, excellent heat resistance and chemical stability, and are not easy to bond with metals. Ceramic cutting tools play a very important role in CNC machining, and have become one of the main cutting tools for high-speed cutting and difficult to machine materials. Ceramic cutting tools are widely used in high-speed cutting, dry cutting, hard cutting, and cutting of difficult to machine materials. Ceramic cutting tools can efficiently process high hardness materials that cannot be processed by traditional cutting tools, achieving "turning instead of grinding"; The optimal cutting speed of ceramic cutting tools can be 2 to 10 times higher than that of hard alloy cutting tools, greatly improving the production efficiency of cutting; The main raw materials used for ceramic cutting tools are the most abundant elements in the earth's crust. Therefore, the promotion and application of ceramic cutting tools is of great significance for improving productivity, reducing processing costs, and saving strategic precious metals. It will also greatly promote the progress of cutting technology.
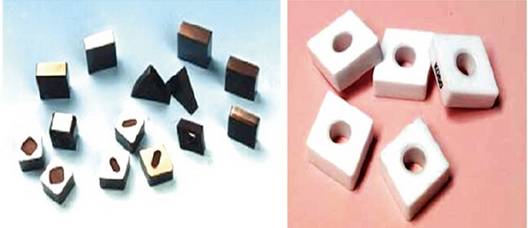
⑴ Types of ceramic tool materials
The types of ceramic tool materials can generally be divided into three categories: alumina based ceramics, silicon nitride based ceramics, and composite silicon nitride alumina based ceramics. Among them, alumina based and silicon nitride based ceramic tool materials are the most widely used. The performance of silicon nitride based ceramics is superior to that of alumina based ceramics.
⑵ Performance and characteristics of ceramic cutting tools
The performance characteristics of ceramic cutting tools are as follows:
① High hardness and good wear resistance: Although the hardness of ceramic cutting tools is not as high as PCD and PCBN, it is significantly higher than that of hard alloy and high-speed steel cutting tools, reaching 93-95HRA. Ceramic cutting tools can process high hard materials that are difficult to machine with traditional tools, making them suitable for high-speed cutting and hard cutting.
② High temperature resistance and good heat resistance: Ceramic cutting tools can still cut at high temperatures above 1200 ℃. Ceramic cutting tools have excellent high-temperature mechanical properties, and the oxidation resistance of A12O3 ceramic cutting tools is particularly good. Even when the cutting edge is in a red hot state, it can be used continuously. Therefore, ceramic cutting tools can achieve dry cutting, thereby saving cutting fluid.
③ Good chemical stability: Ceramic cutting tools are not easy to bond with metals, and are corrosion-resistant with good chemical stability, which can reduce the adhesive wear of cutting tools.
④ Low friction coefficient: Ceramic cutting tools have a low affinity with metals, resulting in a low friction coefficient that can reduce cutting force and cutting temperature.
⑶ Ceramic knives have applications
Ceramics are one of the tool materials mainly used for high-speed precision machining and semi precision machining. Ceramic cutting tools are suitable for cutting various cast iron (gray cast iron, ductile iron, malleable cast iron, cold hard cast iron, high alloy wear-resistant cast iron) and steel (carbon structural steel, alloy structural steel, high-strength steel, high manganese steel, quenched steel, etc.), and can also be used to cut copper alloys, graphite, engineering plastics, and composite materials.
Ceramic tool materials have problems with low bending strength and poor impact toughness, making them unsuitable for cutting at low speeds and under impact loads.
4. Performance and characteristics of coated tool materials and application of tools
Coating the cutting tools is one of the important ways to improve their performance. The emergence of coated cutting tools has made significant breakthroughs in their cutting performance. Coated cutting tools are those that are coated with one or more layers of refractory compounds with good wear resistance on the tool body with good toughness. They combine the tool matrix with a hard coating, thereby greatly improving the tool performance. Coated cutting tools can improve machining efficiency, improve machining accuracy, extend tool life, and reduce machining costs.
About 80% of the cutting tools used in new CNC machine tools use coated tools. Coated cutting tools will be the most important tool variety in the field of CNC machining in the future.
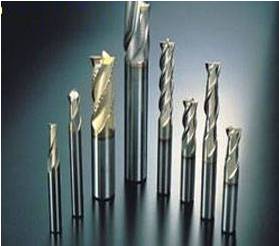
⑴ Types of coated cutting tools
According to different coating methods, coated tools can be divided into chemical vapor deposition (CVD) coated tools and physical vapor deposition (PVD) coated tools. Coated hard alloy cutting tools generally use chemical vapor deposition method, with a deposition temperature of around 1000 ℃. Coated high-speed steel cutting tools generally use physical vapor deposition method, with a deposition temperature of around 500 ℃;
According to the different substrate materials of coated tools, coated tools can be divided into hard alloy coated tools, high-speed steel coated tools, and coated tools on ceramics and superhard materials (diamond and cubic boron nitride).
According to the properties of coating materials, coated tools can be divided into two categories, namely "hard" coated tools and "soft" coated tools. The main goal pursued by "hard" coated cutting tools is high hardness and wear resistance, with the main advantages of high hardness and good wear resistance, typical of which are TiC and TiN coatings. The goal pursued by "soft" coated tools is low friction coefficient, also known as self-lubricating tools. Its friction coefficient with the workpiece material is very low, only about 0.1, which can reduce adhesion, reduce friction, and lower cutting force and cutting temperature.
Recently, nano coating tools have been developed. This coated tool can use different combinations of coating materials (such as metal/metal, metal/ceramic, ceramic/ceramic, etc.) to meet different functional and performance requirements. A well-designed nano coating can endow tool materials with excellent anti friction, anti-wear properties, and self-lubricating properties, making them suitable for high-speed dry cutting.
Characteristics of coated cutting tools
The performance characteristics of coated cutting tools are as follows:
① Good mechanical and cutting performance: Coated cutting tools combine the excellent properties of the substrate and coating materials, maintaining good toughness and high strength of the substrate, as well as high hardness, wear resistance, and low friction coefficient of the coating. Therefore, the cutting speed of coated tools can be increased by more than twice compared to uncoated tools, and higher feed rates are allowed. The lifespan of coated cutting tools has also been improved.
② Strong versatility: Coated tools have a wide range of versatility and significantly expand the processing range. One coated tool can replace several non coated tools.
③ Coating thickness: As the coating thickness increases, the tool life also increases, but when the coating thickness reaches saturation, the tool life no longer increases significantly. When the coating is too thick, it is easy to cause peeling; When the coating is too thin, the wear resistance is poor.
④ Regrindability: Coated blades have poor Regrindability, complex coating equipment, high process requirements, and long coating time.
⑤ Coating materials: Cutting tools with different coating materials have different cutting performance. For example, during low-speed cutting, TiC coating has an advantage; TiN is more suitable for high-speed cutting.
Application of coated cutting tools
Coated cutting tools have great potential in the field of CNC machining and will be the most important tool variety in the future. Coating technology has been applied to end mills, reamers, drill bits, composite hole processing tools, gear hobbing cutters, gear hobbing cutters, gear shaving cutters, forming broaches, and various machine clamp indexable inserts, meeting the needs of high-speed cutting of various materials such as steel and cast iron, heat-resistant alloys, and non-ferrous metals.
5. Types, properties, characteristics, and applications of hard alloy cutting tool materials
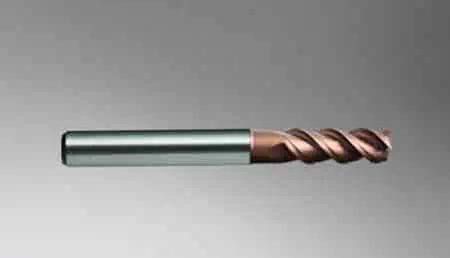
Hard alloy cutting tools, especially indexable hard alloy cutting tools, are the leading products of CNC machining tools. Since the 1980s, various types of integral and indexable hard alloy cutting tools or blades have expanded to various cutting tool fields. Among them, indexable hard alloy cutting tools have expanded from simple turning tools and face milling cutters to various precision, complex, and formed tool fields.
⑴ Types of hard alloy cutting tools
According to the main chemical composition, hard alloys can be divided into tungsten carbide based hard alloys and titanium carbide (TiC (N)) based hard alloys.
Tungsten carbide based hard alloys include three types: tungsten cobalt (YG), tungsten cobalt titanium (YT), and rare carbides added (YW), each with its own advantages and disadvantages. The main components are tungsten carbide (WC), titanium carbide (TiC), tantalum carbide (TaC), niobium carbide (NbC), etc. The commonly used metal bonding phase is Co.
Carbon (nitrogen) titanium based hard alloy is a hard alloy mainly composed of TiC (some with the addition of other carbides or nitrides), and the commonly used metal bonding phases are Mo and Ni.
ISO (International Organization for Standardization) divides cutting hard alloys into three categories:
K-class, including Kl0-K40, is equivalent to YG class in China (mainly composed of WC. Co).
P-class, including P01-P50, is equivalent to YT class in China (mainly composed of WC. TiC. Co).
M class, including M10~M40, is equivalent to YW class in China (mainly composed of WC TiC TaC (NbC) - Co).
A series of alloys ranging from high hardness to maximum toughness are represented by numbers between 01 and 50 for each grade.
⑵ Performance characteristics of hard alloy cutting tools
The performance characteristics of hard alloy cutting tools are as follows:
① High hardness: Hard alloy cutting tools are made by powder metallurgy of carbides (called hard phases) and metal binders (called bonding phases) with high hardness and melting point. Their hardness reaches 89-93HRA, which is much higher than that of high-speed steel. At 5400C, their hardness can still reach 82-87HRA, which is the same as that of high-speed steel at room temperature (83-86HRA). The hardness value of hard alloys varies with the properties, quantity, particle size, and content of metal bonding phases of carbides, and generally decreases with an increase in the content of bonding metal phases. When the adhesive phase content is the same, the hardness of YT type alloys is higher than that of YG type alloys, and alloys with added TaC (NbC) have higher high-temperature hardness.
② Bending strength and toughness: The bending strength of commonly used hard alloys ranges from 900 to 1500MPa. The higher the content of metal bonding phase, the higher the bending strength. When the adhesive content is the same, the strength of YG type (WC Co) alloy is higher than that of YT type (WC TiC Co) alloy, and the strength decreases with the increase of TiC content. Hard alloy is a brittle material, and its impact toughness at room temperature is only 1/30-1/8 of that of high-speed steel.
Application of commonly used hard alloy cutting tools
YG type alloys are mainly used for processing cast iron, non-ferrous metals, and non-metallic materials. Fine grained hard alloys (such as YG3X, YG6X) have higher hardness and wear resistance than medium grained hard alloys when their cobalt content is the same. They are suitable for processing special hard cast iron, austenitic stainless steel, heat-resistant alloys, titanium alloys, hard bronze, and wear-resistant insulation materials.
The outstanding advantages of YT type hard alloys are high hardness, good heat resistance, higher hardness and compressive strength at high temperatures compared to YG type, and good oxidation resistance. Therefore, when it is required that the knife has high heat resistance and wear resistance, a grade with a higher TiC content should be selected. YT type alloys are suitable for processing plastic materials such as steel, but are not suitable for processing titanium alloys or silicon aluminum alloys.
YW type alloys possess the properties of YG and YT types of alloys, with good comprehensive performance. They can be used for processing steel materials, as well as for processing cast iron and non-ferrous metals. If the cobalt content is appropriately increased, this type of alloy can have high strength and can be used for rough machining and intermittent cutting of various difficult to machine materials.
6. Types, characteristics, and applications of high-speed steel cutting tools
High Speed Steel (HSS) is a type of high alloy tool steel that contains a significant amount of alloying elements such as W, Mo, Cr, and V. High speed steel cutting tools have excellent comprehensive performance in terms of strength, toughness, and processability. In complex cutting tools, especially in manufacturing hole processing tools, milling cutters, thread cutting tools, drawing cutters, gear cutting tools, and other complex edge shaped cutting tools, high-speed steel still occupies the main position. High speed steel cutting tools are easy to grind sharp cutting edges.
According to different uses, high-speed steel can be divided into general-purpose high-speed steel and high-performance high-speed steel.
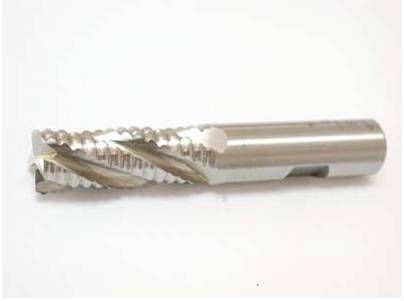
⑴ Universal high-speed steel cutting tools
Universal high-speed steel. Generally, it can be divided into two categories: tungsten steel and tungsten molybdenum steel. This type of high-speed steel contains (C) ranging from 0.7% to 0.9%. According to the different tungsten content in steel, it can be divided into tungsten steel with a W content of 12% or 18%, tungsten molybdenum steel with a W content of 6% or 8%, and molybdenum steel with a W content of 2% or no W. Universal high-speed steel has a certain hardness (63-66HRC) and wear resistance, high strength and toughness, good plasticity and processability, and is widely used in the manufacturing of various complex cutting tools.
① Tungsten steel: The typical grade of general-purpose high-speed steel tungsten steel is W18Cr4V, (referred to as W18), which has good comprehensive properties and a high temperature hardness of 48.5HRC at 6000C. It can be used to manufacture various complex cutting tools. It has advantages such as good grindability and low decarburization sensitivity, but due to the high content of carbides, uneven distribution, larger particles, and low strength and toughness.
② Tungsten molybdenum steel: refers to a high-speed steel obtained by replacing a portion of tungsten in tungsten steel with molybdenum. The typical grade of tungsten molybdenum steel is W6Mo5Cr4V2, abbreviated as M2. The carbide particles of M2 are small and uniform, with better strength, toughness, and high-temperature plasticity than W18Cr4V. Another type of tungsten molybdenum steel is W9Mo3Cr4V (abbreviated as W9), which has slightly higher thermal stability than M2 steel, better bending strength and toughness than W6M05Cr4V2, and has good machinability.
⑵ High performance high-speed steel cutting tools
High performance high-speed steel refers to a new type of steel that adds some carbon and vanadium content, as well as alloy elements such as Co and Al, to the composition of general-purpose high-speed steel, in order to improve its heat resistance and wear resistance. There are mainly the following categories:
① High carbon high-speed steel. High carbon high-speed steel (such as 95W18Cr4V) has high hardness at room temperature and high temperature, making it suitable for manufacturing and processing ordinary steel and cast iron, drill bits, reamers, taps, and milling cutters with high wear resistance requirements, or cutting tools for processing harder materials. It is not suitable to withstand large impacts.
② High vanadium high-speed steel. Typical grades, such as W12Cr4V4Mo (referred to as EV4), increase the V content to 3% -5%, have good wear resistance, and are suitable for cutting materials that cause significant tool wear, such as fibers, hard rubber, plastics, etc. They can also be used for processing materials such as stainless steel, high-strength steel, and high-temperature alloys.
③ Cobalt high-speed steel. It belongs to cobalt containing superhard high-speed steel, with a typical grade such as W2Mo9Cr4VCo8 (referred to as M42), which has high hardness and can reach 69-70HRC. It is suitable for processing high-strength heat-resistant steel, high-temperature alloys, titanium alloys and other difficult to machine materials. M42 has good grindability and is suitable for making precision and complex cutting tools, but it is not suitable for working under impact cutting conditions.
④ Aluminum high-speed steel. It belongs to aluminum containing superhard high-speed steel, with typical grades such as W6Mo5Cr4V2Al (referred to as 501). The high-temperature hardness at 6000C also reaches 54HRC, and the cutting performance is equivalent to M42. It is suitable for manufacturing milling cutters, drill bits, reamers, gear cutting tools, broaches, etc., and is used for processing alloy steel, stainless steel, high-strength steel, and high-temperature alloys.
⑤ Nitrogen superhard high-speed steel. A typical grade, such as W12M03Cr4V3N, abbreviated as V3N, is a nitrogen containing superhard high-speed steel with hardness, strength, and toughness comparable to M42. It can be used as a substitute for cobalt containing high-speed steel for low-speed cutting of difficult to machine materials and low-speed high-precision machining.
⑶ Melting high-speed steel and powder metallurgy high-speed steel
According to different manufacturing processes, high-speed steel can be divided into melted high-speed steel and powder metallurgy high-speed steel.
① Melting high-speed steel: Both ordinary high-speed steel and high-performance high-speed steel are manufactured using the melting method. They are made into cutting tools through processes such as smelting, ingot casting, and plating and rolling. The serious problem that is prone to occur during the melting of high-speed steel is carbide segregation. Hard and brittle carbides are unevenly distributed in high-speed steel, and the grain size is coarse (up to tens of micrometers), which has adverse effects on the wear resistance, toughness, and cutting performance of high-speed steel cutting tools.
② Powder Metallurgical High Speed Steel (PM HSS): Powder Metallurgical High Speed Steel (PM HSS) is a steel liquid melted in a high-frequency induction furnace, which is atomized with high-pressure argon or pure nitrogen gas, and then rapidly cooled to obtain a small and uniform crystalline structure (high-speed steel powder). The resulting powder is then pressed into a cutting tool blank at high temperature and pressure, or first made into a steel billet and then forged and rolled into a cutting tool shape. Compared with high-speed steel manufactured by melting method, PM HSS has the advantages of small and uniform carbide grains, significantly improved strength, toughness, and wear resistance compared to melted high-speed steel. PM HSS tools will further develop and occupy an important position in the field of complex CNC tools. Typical grades, such as F15, FR71, GFl, GF2, GF3, PT1, PVN, etc., can be used to manufacture large-sized, heavy-duty, and impact resistant cutting tools, as well as precision cutting tools.
III The selection principles of CNC tool materials
The widely used CNC tool materials currently include diamond tools, cubic boron nitride tools, ceramic tools, coated tools, hard alloy tools, and high-speed steel tools. There are many general grades of cutting tool materials, and their performance varies greatly. The main performance indicators of various tool materials are shown in the table below.
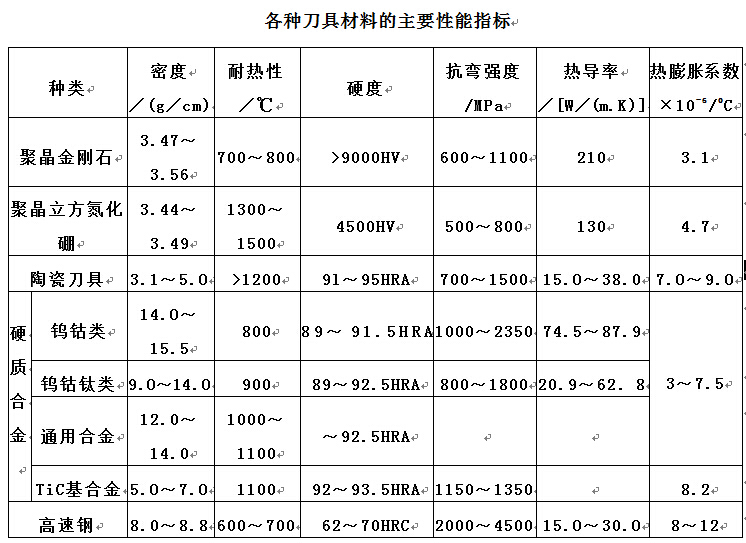
The selection of cutting tool materials for CNC machining must be based on the workpiece being processed and the machining properties. The selection of tool materials should be reasonably matched with the machining object. The matching of cutting tool materials with the machining object mainly refers to the matching of their mechanical, physical, and chemical properties, in order to achieve the longest tool life and maximum cutting productivity.
1. Matching of mechanical properties between cutting tool materials and machining objects
The mechanical performance matching problem between cutting tools and machining objects mainly refers to the matching of mechanical performance parameters such as strength, toughness, and hardness between the tools and workpiece materials. The cutting tool materials with different mechanical properties are suitable for processing different workpiece materials.
① The hardness order of tool materials is: diamond tools>cubic boron nitride tools>ceramic tools>hard alloys>high-speed steel.
② The order of bending strength of tool materials is: high-speed steel>hard alloy>ceramic tools>diamond and cubic boron nitride tools.
③ The order of toughness of tool materials is: high-speed steel>hard alloy>cubic boron nitride, diamond, and ceramic tools.
High hardness workpiece materials must be processed with higher hardness cutting tools, and the hardness of the cutting tool material must be higher than that of the workpiece material, generally requiring a hardness of 60HRC or above. The higher the hardness of the tool material, the better its wear resistance. For example, as the cobalt content in hard alloys increases, their strength and toughness increase, while hardness decreases, making them suitable for rough machining; When the cobalt content decreases, its hardness and wear resistance increase, making it suitable for precision machining.
Tools with excellent high-temperature mechanical properties are particularly suitable for high-speed cutting. The excellent high-temperature performance of ceramic cutting tools enables them to cut at a high speed, and the allowable cutting speed can be increased by 2-10 times compared to hard alloys.
2. Matching the physical properties of cutting tool materials and machining objects
Tools with different physical properties, such as high-speed steel tools with high thermal conductivity and low melting point, ceramic tools with high melting point and low thermal expansion, and diamond tools with high thermal conductivity and low thermal expansion, are suitable for processing different workpiece materials. When processing workpieces with poor thermal conductivity, tool materials with good thermal conductivity should be used to quickly transfer cutting heat and reduce cutting temperature. Diamond, due to its high thermal conductivity and thermal diffusion rate, is prone to dissipate cutting heat and does not produce significant thermal deformation, which is particularly important for precision machining tools that require high dimensional accuracy.
① The heat resistance temperature of various cutting tool materials: 700-8000C for diamond cutting tools, 13000-15000C for PCBN cutting tools, 1100-12000C for ceramic cutting tools, 900-11000C for TiC (N) based hard alloys, 800-9000C for WC based ultrafine grain hard alloys, and 600-7000C for HSS.
② The thermal conductivity order of various tool materials is: PCD>PCBN>WC based hard alloy>TiC (N) based hard alloy>HSS>Si3N4 based ceramic>A1203 based ceramic.
③ The order of thermal expansion coefficients for various tool materials is: HSS>WC based hard alloy>TiC (N)>A1203 based ceramic>PCBN>Si3N4 based ceramic>PCD.
④ The order of thermal shock resistance of various tool materials is: HSS>WC based hard alloy>Si3N4 based ceramic>PCBN>PCD>TiC (N) based hard alloy>A1203 based ceramic.
3. Matching of chemical properties between cutting tool materials and machining objects
The chemical performance matching problem between cutting tool materials and machining objects mainly refers to the matching of chemical performance parameters such as chemical affinity, chemical reaction, diffusion, and dissolution between tool materials and workpiece materials. The cutting tools with different materials are suitable for processing different workpiece materials.
① The temperature resistance of various cutting tool materials to adhesion (compared to steel) is as follows: PCBN>ceramic>hard alloy>HSS.
② The oxidation resistance temperature of various tool materials is as follows: ceramic>PCBN>hard alloy>diamond>HSS.
③ The diffusion strength of different cutting tool materials (for steel) is: diamond>Si3N4 based ceramics>PCBN>A1203 based ceramics. The diffusion intensity (for titanium) is: A1203 based ceramics>PCBN>SiC>Si3N4>diamond.
4. Reasonable selection of CNC tool materials
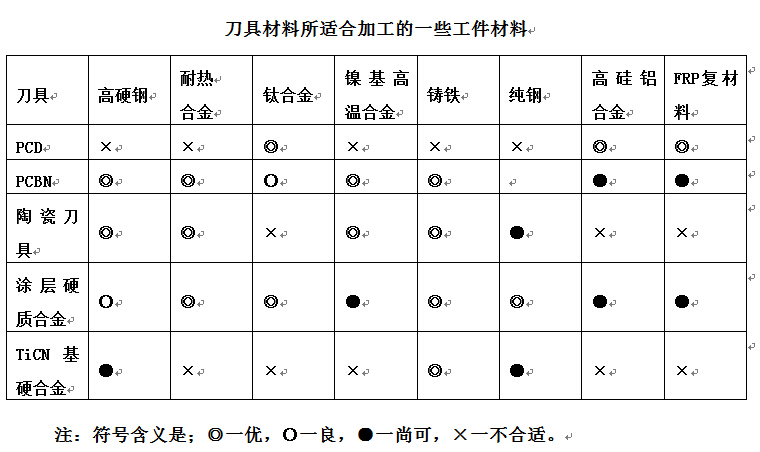
Generally speaking, PCBN, ceramic cutting tools, coated hard alloys, and TiCN based hard alloy cutting tools are suitable for CNC machining of black metals such as steel; PCD tools are suitable for processing non-ferrous metal materials such as Al, Mg, Cu, as well as their alloys and non-metallic materials. Table 3-3-2 lists some workpiece materials suitable for machining with the aforementioned tool materials.
The following table lists some workpiece materials that are suitable for processing with various tool materials.