


Have you learned positioning and clamping, as well as machining?
In the process of encountering various solutions, we have found that there are always some positioning and clamping problems that are not well solved in the preliminary design. In this way, even the most innovative solutions will lose practical significance. Understanding the basic knowledge of positioning and clamping can fundamentally ensure the integrity of fixture design and processing plans.
Locator knowledge
1, The basic principle of positioning from the side of the workpiece
When positioning from the side of the workpiece, like the support, the 3-point principle is the most basic principle. This is the same principle as the support element, known as the 3-point principle, derived from the principle of determining a plane from three points that are not on the same line. Among the four points, three can determine a face, so a total of four faces can be determined. However, no matter how it is located, it is quite difficult to make the fourth point in the same plane.
▲ Three point principle
For example, when using four fixed height locators, only three points at a certain point can contact the workpiece, and the possibility of the remaining fourth point not touching the workpiece is still high.
So, when configuring a locator, it is generally based on three points and the distance between these three points should be increased as much as possible.
In addition, when configuring the locator, it is necessary to confirm in advance the direction of the applied processing load. The direction of the machining load, also known as the travel direction of the tool holder/tool, can directly affect the overall accuracy of the workpiece by configuring a locator at the end of the feed direction.
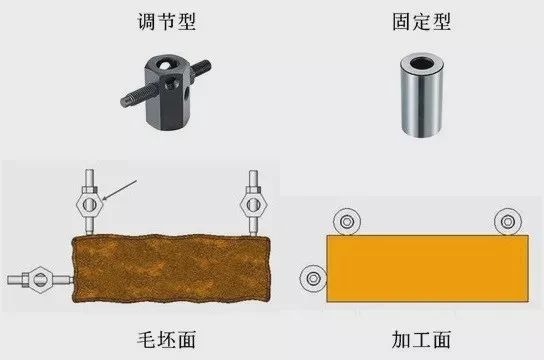
Generally, bolt type adjustable locators are used for positioning on the workpiece blank surface, and fixed type (workpiece contact surface ground) locators are used for positioning on the workpiece machining surface.
2, Basic principles for locating workpiece holes
When using the holes processed in the previous process of the workpiece for positioning, it is necessary to use pins with tolerances for positioning. By combining the accuracy of the workpiece hole with the accuracy of the pin shape, and based on the fit tolerance, the positioning accuracy can meet the actual requirements.
In addition, when using a pin for positioning, one usually uses a straight pin and the other uses a diamond pin. This makes it more convenient to assemble and disassemble the workpiece, and it is rare for the workpiece to get stuck with the pin.
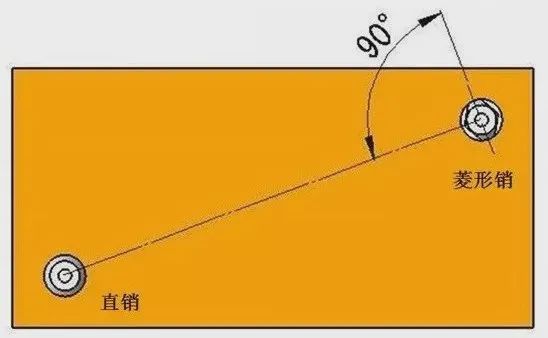
▲ Use pin positioning
Of course, it is also possible to use straight pins for both pins by adjusting the fit tolerance. For more precise positioning, a straight pin and a diamond pin are usually the most effective.
When using a straight pin and a diamond pin, the configuration direction of the diamond pin (at the point of contact with the workpiece) is usually perpendicular to the line connecting the straight pin and diamond pin at a 90 ° angle. This configuration method is for angular positioning (in the direction of workpiece rotation).
Related knowledge of clamps
1, Classification of Clamping Devices
According to the clamping direction, it is generally divided into the following categories:
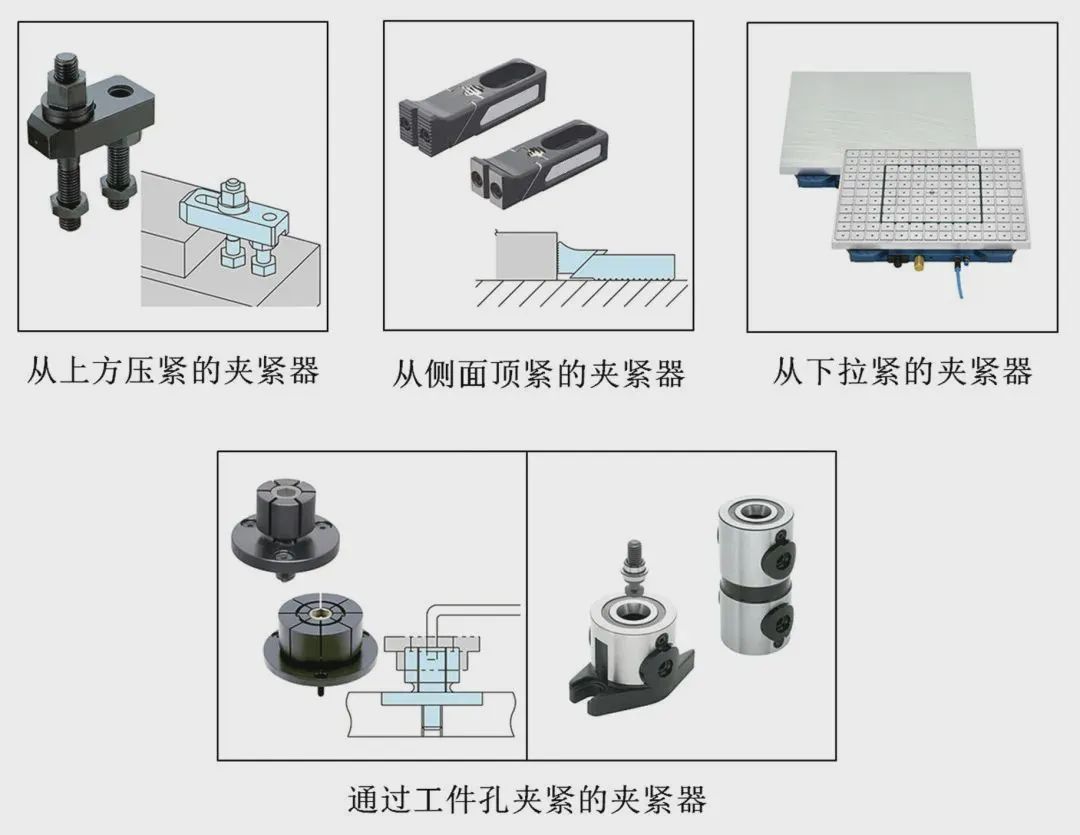
Next, let's take a look at the characteristics of various clamps.
1. Clamping device pressed from above
The clamping device that presses from above the workpiece has the least deformation during clamping and is the most stable during workpiece processing. Therefore, in general, the first consideration is to clamp from above the workpiece. The most common fixture for pressing from above the workpiece is a manual mechanical fixture. For example, the following diagram is called a "pine leaf type" clamp. The clamping device composed of a pressure plate, double headed bolts, jack, and nut is called a "loose leaf type" clamping device.
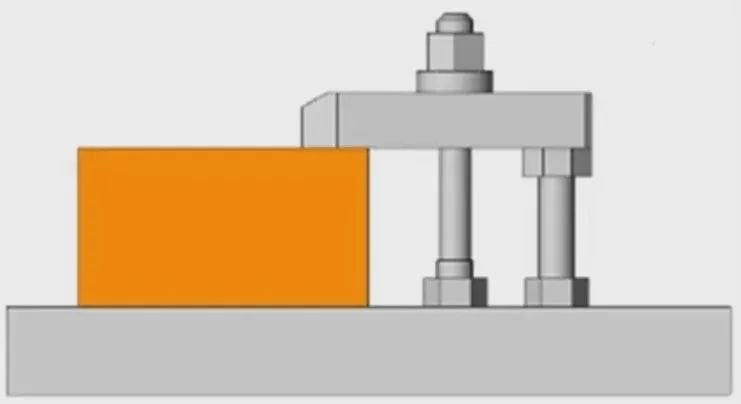
In addition, different shapes of pressure plates can be selected according to the shape of the workpiece, corresponding to various shapes of the workpiece.
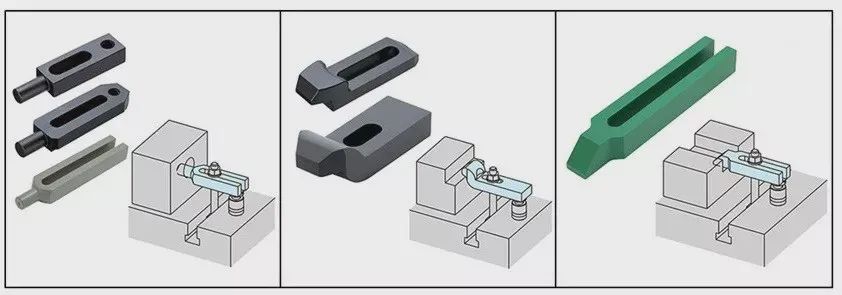
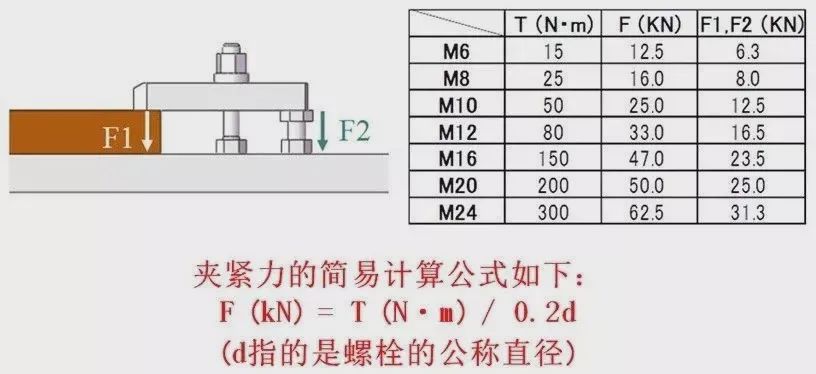
The relationship between the torque and clamping force of the pine leaf clamp during clamping can be calculated by the pushing force of the bolt.
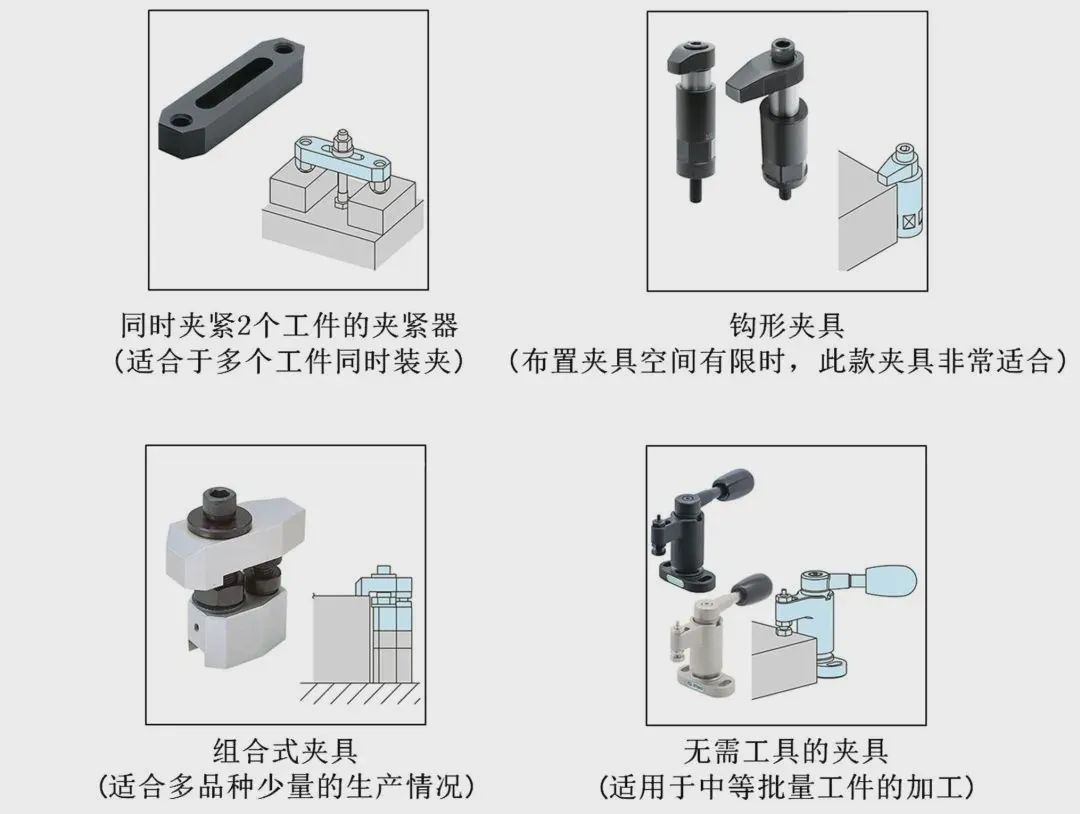
In addition to the loose leaf type clamp, there are also similar clamps for clamping from above the workpiece.
2. Clamping device for clamping from the side
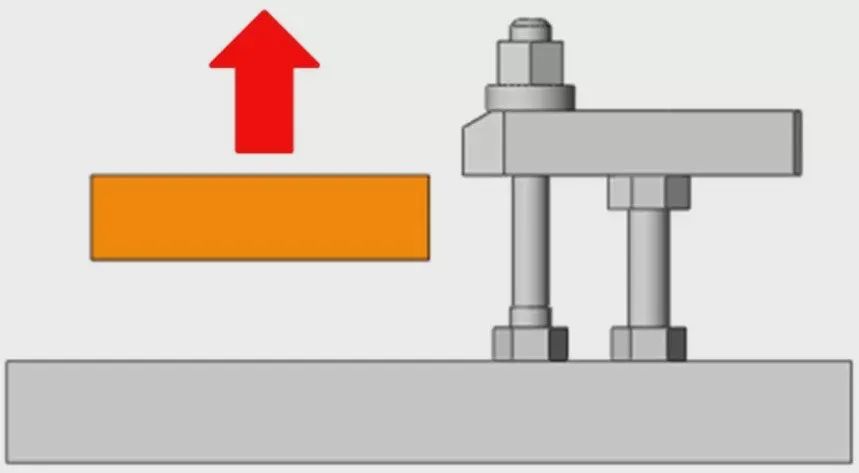
Originally, the clamping method of clamping the workpiece from above is the most stable in accuracy and the minimum processing load on the workpiece. However, in various situations where machining is required above the workpiece or clamping from above is not very suitable, which makes it impossible to clamp from above the workpiece, it is possible to choose to clamp from the side of the workpiece. However, when clamping the workpiece from the side, it will generate an upward force, and how to eliminate this force must be taken into consideration when designing the fixture.
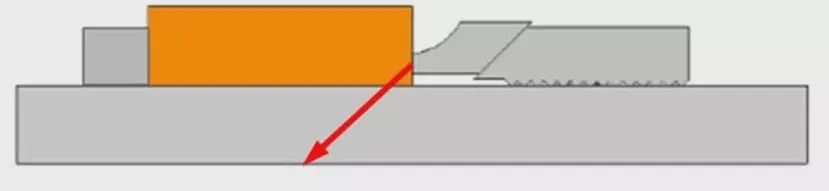
Clamping devices that clamp from the side also have a downward force while generating thrust from the side, as shown in the above figure. This type of fixture can effectively prevent the workpiece from floating up.
There are also similar clamps for clamping from the side.
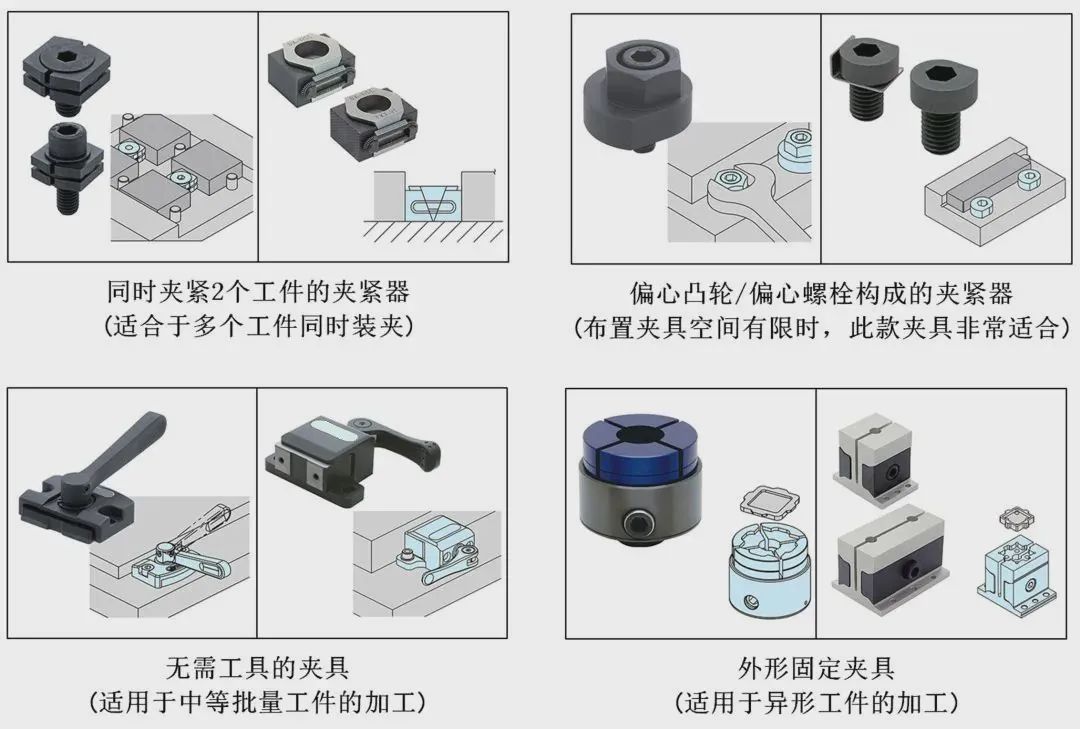
3. Clamp the workpiece tightly from the pull down position
When processing the upper surface of a thin plate workpiece, not only cannot it be clamped from above, but it is also unreasonable to press it from the side. The only reasonable clamping method is to tighten the workpiece from below. When tightening the workpiece from below, if it is made of iron material, a magnetic clamp can usually be used. When using non-ferrous metal workpieces, vacuum suction cups can generally be used to tighten them.
In the above two cases, the clamping force is directly proportional to the contact area between the workpiece and the magnet or vacuum suction cup. If the machining load is too high when processing small workpieces, the machining effect will not be ideal.
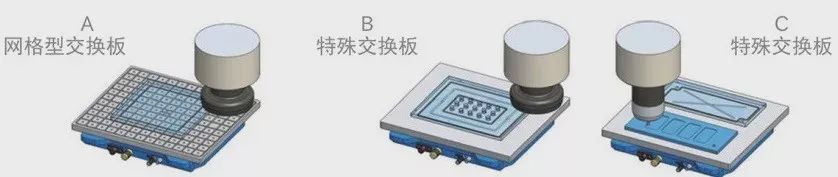
In addition, when using magnets or vacuum suction cups, the contact surface between the magnet and the vacuum suction cup needs to be smoothed to a certain degree in order to be used safely and normally.
4. Clamping device using hole clamping
When using a 5-axis machining machine for multi face simultaneous processing or mold processing, in order to prevent the influence of fixtures and tools on the processing, it is generally more appropriate to choose to use hole clamping. Compared with clamping from above and from the side of the workpiece, using hole clamping generates less load on the workpiece and can effectively deform it.
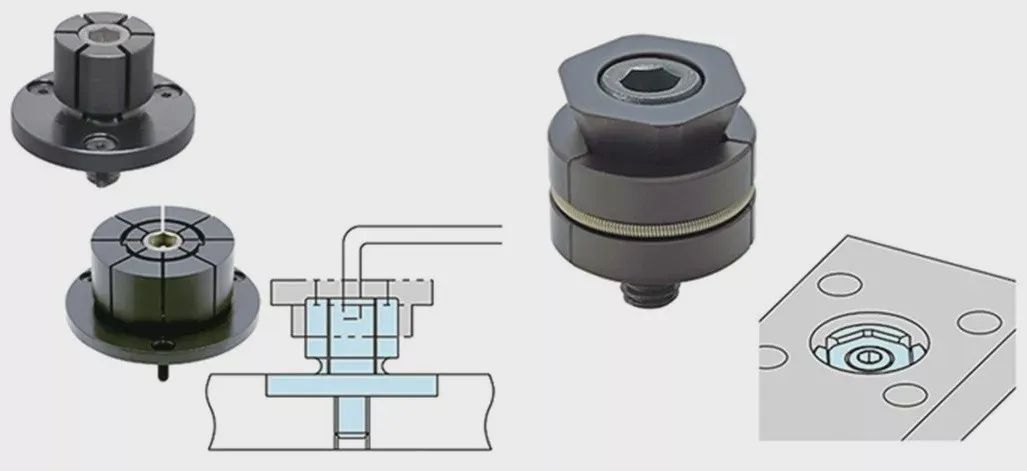
▲ Using holes for direct processing
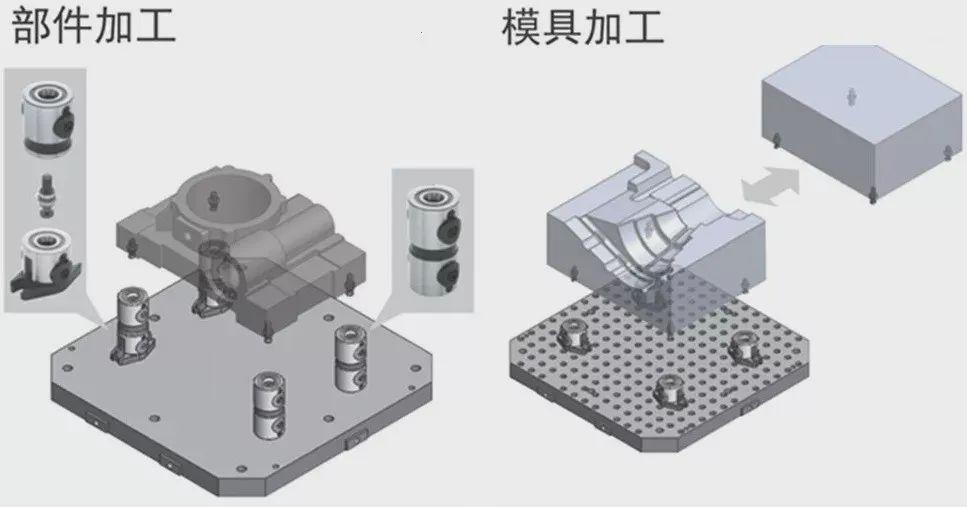
▲ Set pull pins for clamping
2, Pre clamping
The above mainly refers to fixtures for workpiece clamping, and it is also crucial to improve operability and enhance the use of pre clamping. When setting the workpiece vertically on the base, the workpiece will fall due to gravity. At this point, it is necessary to operate the gripper while holding down the workpiece with your hands.
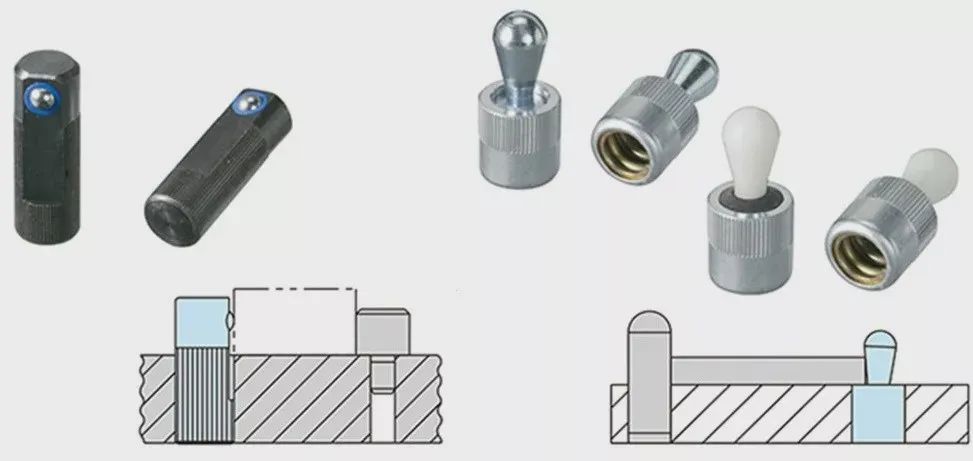
▲ Pre clamping
If the workpiece is of large weight or when multiple pieces are clamped simultaneously, the operability will be greatly reduced, and the clamping time will also be long. At this point, using this spring type pre clamping product can enable the workpiece to operate the clamp in a stationary state, greatly improving operability and reducing workpiece clamping time.
3, Precautions when selecting clamps
When using multiple types of clamps within the same fixture, the tools used for clamping and loosening must be consistent. For example, as shown in the left figure, when using multiple tool wrenches for clamping operations, the overall burden on the operator will increase, and the overall clamping time of the workpiece will also be longer. For example, in the image on the right, unify the tool wrench and bolt size to facilitate on-site operators.
▲ Workpiece clamping operability
In addition, when configuring the clamping device, it is necessary to consider the operability of workpiece clamping as much as possible. If the workpiece needs to be tilted during clamping, it will be inconvenient to operate. When designing fixtures and fixtures, it is necessary to avoid this situation.


