Dry goods | How to reduce vibration during milling process?
In milling, vibration may occur due to the limitations of cutting tools, tool holders, machine tools, workpieces, or fixtures. To reduce vibration, some strategies need to be considered.
01 Cutting tools
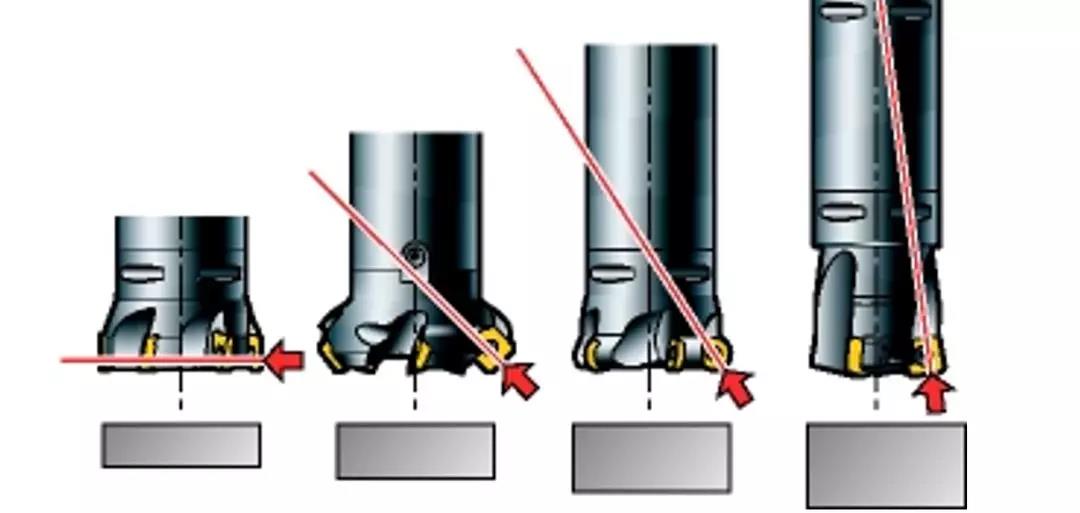
1) For surface milling, the direction of cutting force must be considered:
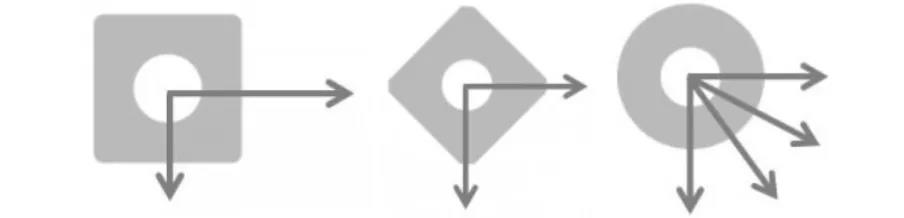
When using a 90 ° milling cutter, the cutting force is mainly concentrated in the radial direction. Under long overhanging conditions, this will cause the milling cutter to sway; However, when milling thin-walled/vibration sensitive parts, low axial forces are advantageous
45 ° milling cutter can generate uniformly distributed axial and radial forces
The circular blade milling cutter guides most of the force upwards along the spindle, especially when the cutting depth is small. In addition, the 10 ° milling cutter transfers the main cutting force to the spindle, thereby reducing vibration caused by long tool overhangs
In milling, vibration may occur due to the limitations of cutting tools, tool holders, machine tools, workpieces, or fixtures. To reduce vibration, some strategies need to be considered.
01 Cutting tools
1) For surface milling, the direction of cutting force must be considered:
When using a 90 ° milling cutter, the cutting force is mainly concentrated in the radial direction. Under long overhanging conditions, this will cause the milling cutter to sway; However, when milling thin-walled/vibration sensitive parts, low axial forces are advantageous
45 ° milling cutter can generate uniformly distributed axial and radial forces
The circular blade milling cutter guides most of the force upwards along the spindle, especially when the cutting depth is small. In addition, the 10 ° milling cutter transfers the main cutting force to the spindle, thereby reducing vibration caused by long tool overhangs
02 Knife handle
Using Coromant Capto ® The modular tool holder system can assemble the required length of tools while maintaining high stability and minimal jumping.
1) Maintain the highest possible rigidity and shortest possible length of the tool assembly
2) Choose the largest possible diameter/size of the connecting rod
3) Using Coromant Capto suitable for oversized milling cutters ® Connecting rods, avoid using reduced diameter connecting rods
4) For small-sized milling cutters, if possible, use tapered extension rods
5) In the final process where the cutting tool is located deep in the part, an extended cutting tool is used at the predetermined position. Adjust cutting parameters based on the length of each tool
6) If the spindle speed exceeds 20000 rpm, use dynamically balanced cutting tools and tool holders

Oversized milling cutter
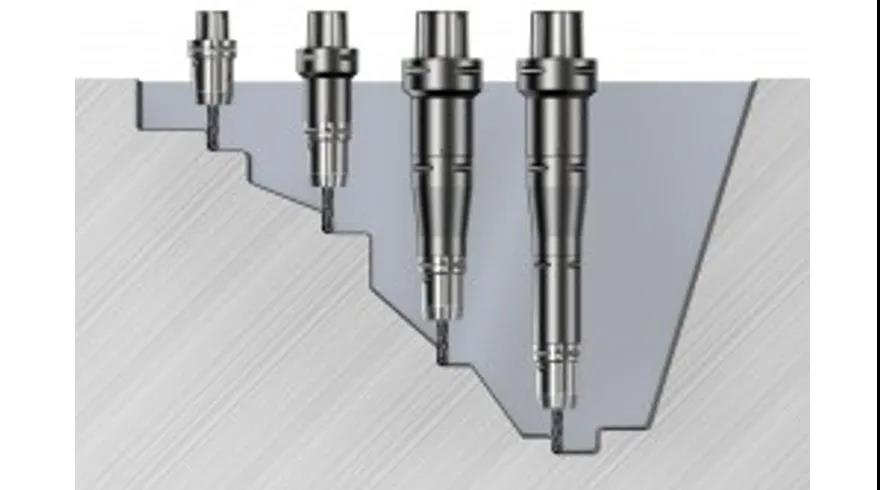
Be sure to use the shortest possible tool length and gradually increase the length
03 Vibration reducing milling cutter
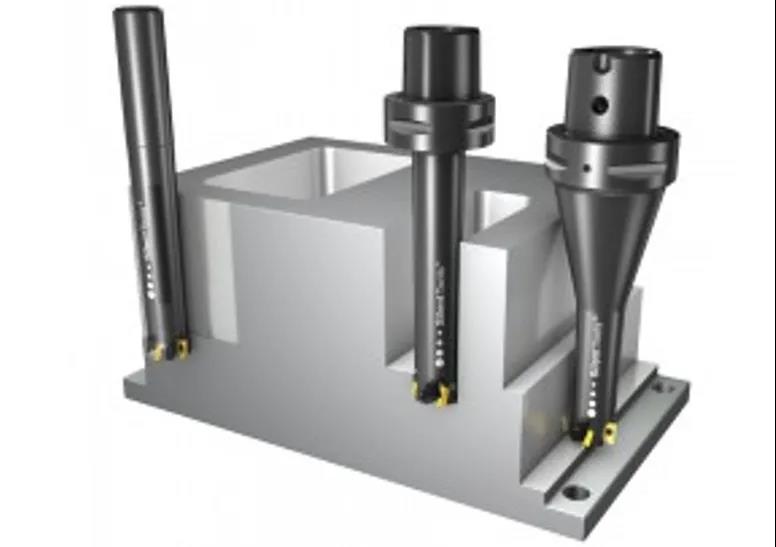
If the overhang is greater than 4 times the tool diameter, the milling vibration trend may become more pronounced, Silent Tools ™ Vibration reducing milling cutters can significantly improve productivity.
04 Cutting edge
To reduce cutting force:
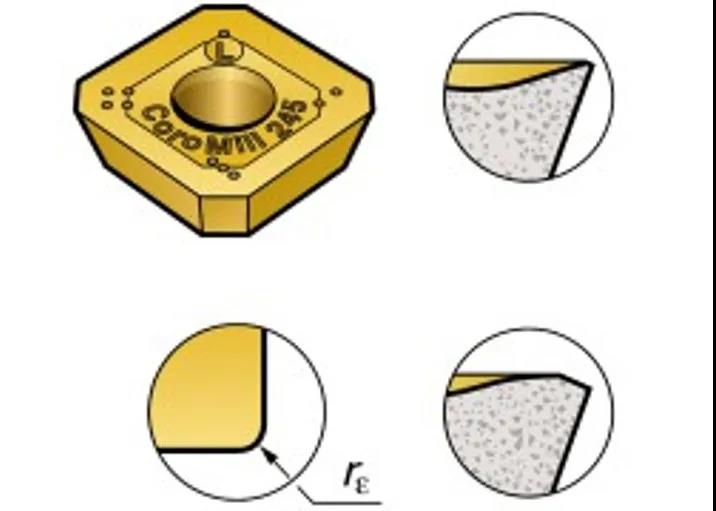
1) Choose a light load groove type L with sharp cutting edges and a thin coating material
2) Use a blade with a small tip radius and a small parallel edge band
Sometimes, the vibration trend can be reduced by adding more damping to the system. Use cutting edge grooves with larger negative rake angles and slightly worn cutting edges.
05 Cutting parameters and tool path programming
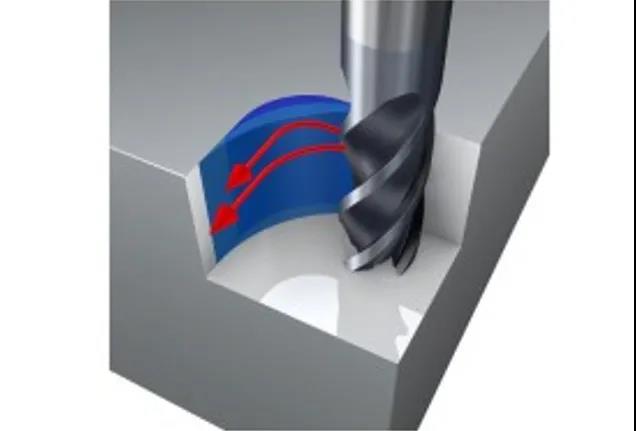
1) Be sure to position the milling cutter relative to the center of the milling surface
2) For KAPR 90 ° long edge milling cutters or end mills, use a small radial cutting depth (maximum ae=25%) × DC) and axial cutting depth (maximum ap=100%) × De)
3) When milling, use small cutting depth ap and high feed fz, as well as circular blades or high feed milling cutters with small main deviation angles
4) To avoid vibration in corners through programming with large arc cutting, refer to inner corner milling
5) If the chip thickness becomes too thin, the cutting edge will scratch instead of cutting, resulting in vibration. In this case, the feed rate per tooth should be increased
06 Machine Tool
The condition of the machine tool may have a significant impact on the trend of milling vibration. Excessive wear of spindle bearings or feed mechanisms will lead to poor machining performance. Carefully choose machining strategies and cutting force directions to fully utilize machine tool stability.
Each machine tool spindle has unstable areas that are prone to vibration. The stable cutting area is described by the stability diagram and increases with the increase of rotational speed. Even a speed increase as low as 50 rpm can transform the cutting process from an unstable state of vibration to a stable state.
07 Workpiece and its fixture
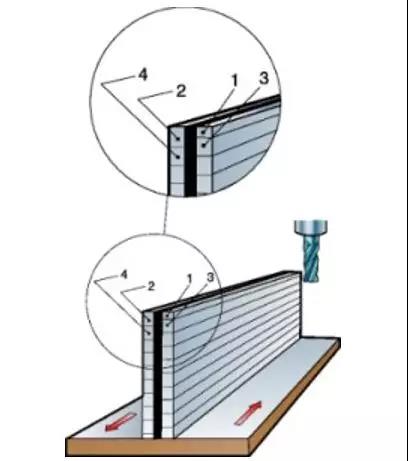
When milling thin-walled/parts with bases, and/or when the fixture rigidity is poor, consider the following points:
1) The fixture should be close to the machine tool workbench
2) Optimize the tool path and feed direction towards the position with the highest strength of the machine tool/fixture to obtain the most stable cutting conditions
3) Avoid machining along the direction where the workpiece is not adequately supported
4) When the rigidity of the fixture and/or workpiece is poor in a specific direction, reverse milling can reduce the trend of vibration
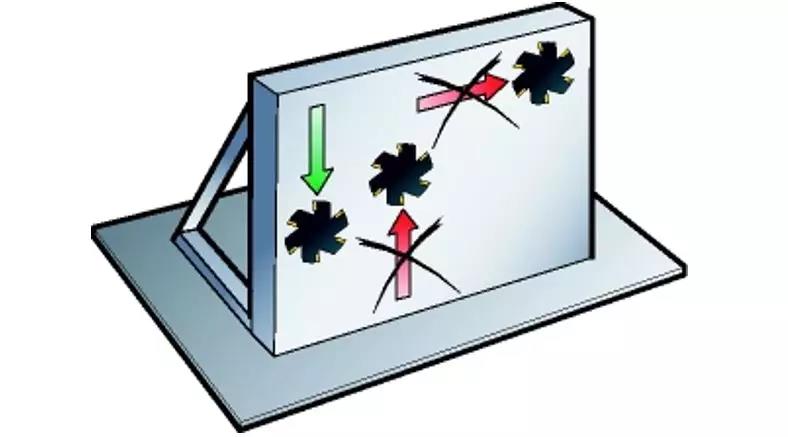
When the rigidity of the fixture is poor, use the feed direction facing the machine tool workbench
Please note that the first cut should be executed at 1/2 of the second cut depth, the second cut should be executed at 1/2 of the third cut depth, and so on.