


【 Manufacturing Technology 】 Selection of milling cutters under complex machining conditions
In cutting machining, in order to maximize machining quality and repetitive accuracy, it is necessary to correctly select and determine suitable cutting tools. For some challenging and difficult machining, the selection of cutting tools is particularly important.
High speed tool path
The CAD/CAM system achieves extremely high cutting accuracy by precisely controlling the cutting arc length in the high-speed cycloidal tool path. When the milling cutter cuts into the corner or other complex geometric shapes, the cutting amount will not increase. In order to fully utilize this technological advancement, tool manufacturers have designed and developed advanced small diameter milling cutters. Small diameter milling cutters can cut more workpiece materials per unit of time and achieve higher metal removal rates by using high-speed tool paths.
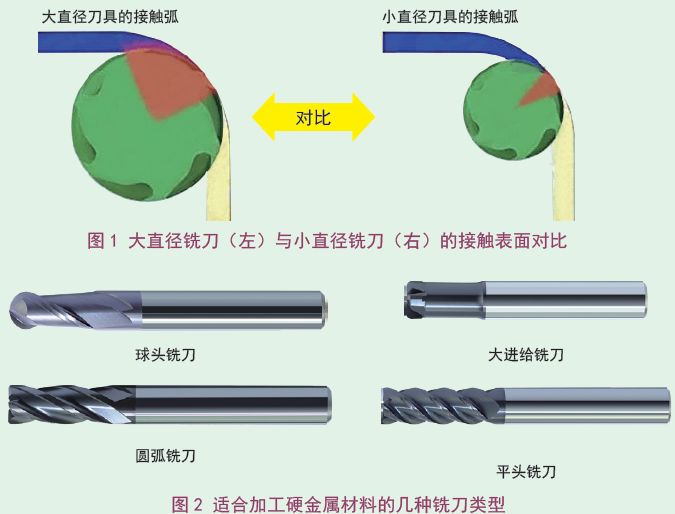
During machining, excessive contact between the tool and the surface of the workpiece can easily lead to tool failure. An effective rule of thumb is to use a milling cutter with a diameter of approximately 1/2 of the narrowest part of the workpiece. When the radius of the milling cutter is smaller than the narrowest part of the workpiece, there is room for the tool to move left and right, and the minimum cutting angle can be obtained. Milling cutters can use more cutting edges and higher feed rates. In addition, when using a milling cutter with a diameter of 1/2 of the narrowest part of the workpiece, a smaller cutting angle can be maintained, and it will not increase when the tool is turned.
The stiffness of the machine tool also helps determine the size of the tool that can be used. For example, when cutting on a 40 degree machine tool, the diameter of the milling cutter should usually be less than 12.7mm. The use of larger diameter milling cutters can generate significant cutting forces that may exceed the machine's load-bearing capacity, leading to vibration, deformation, decreased surface smoothness, and shortened tool life.
When using a newer high-speed tool path, the sound emitted by the milling cutter at the corner is no different from that of straight cutting. The sound emitted by the milling cutter during the cutting process is the same, indicating that it has not been subjected to significant thermal and mechanical impacts. The milling cutter emits a sharp whistling sound every time it turns or cuts into a corner, indicating that it may be necessary to reduce the diameter size of the milling cutter to reduce the cutting angle. The sound produced by cutting remains unchanged, indicating that the cutting pressure borne by the milling cutter is uniform and consistent, and does not fluctuate up and down with changes in the geometric shape of the workpiece, because its cutting angle remains constant.
Milling narrow parts
High feed milling cutters are suitable for milling narrow parts and can generate chip thinning effects, enabling them to perform milling at higher feed rates.
In the processing of spiral milling holes and milling rib plates, the tool inevitably comes into contact with the machining surface. However, using a high feed milling cutter can minimize the surface contact with the workpiece, thereby reducing cutting heat and tool deformation.
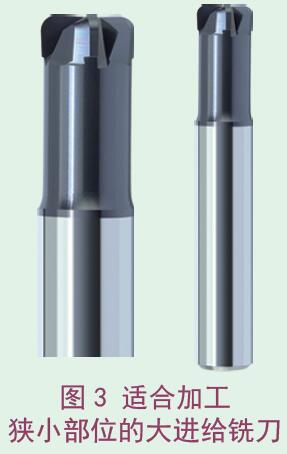
In these two types of machining, the high feed milling cutter is usually in a semi closed state during cutting. Therefore, the maximum radial cutting step should be 25% of the milling cutter diameter, and the maximum Z-cut depth for each cutting should be 2% of the milling cutter diameter. In spiral milling holes, when the milling cutter cuts into the workpiece with a spiral cutting path, the spiral cutting angle is 2 °~3 ° until it reaches a Z-cutting depth of 2% of the milling cutter diameter.
If the high feed milling cutter is in an open state during cutting, its radial cutting step depends on the hardness of the workpiece material. When milling workpiece materials with a hardness of HRC30-50, the maximum radial cutting step should be 5% of the milling cutter diameter; When the material hardness is higher than HRC50, the maximum radial cutting step and the maximum Z-direction cutting depth of each cutting step are both 2% of the milling cutter diameter.
Milling straight walls
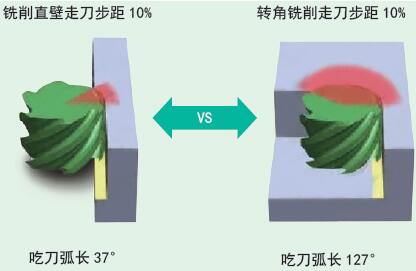
When milling flat ribbed plates or straight walls, using a circular arc milling cutter yields the best results. A 4-6 blade circular arc milling cutter is particularly suitable for profile milling on areas with straight walls or very open areas. The more cutting edges a milling cutter has, the greater the feed rate that can be used. However, machining programmers still need to minimize the surface contact between the tool and the workpiece as much as possible and use smaller radial cutting widths. When machining on machines with poor rigidity, it is advantageous to use a smaller diameter milling cutter, which can reduce surface contact with the workpiece.
The walking distance and cutting depth of the multi edge circular arc milling cutter are the same as those of the high feed milling cutter. Cycloidal tool paths can be used for groove cutting of hardened materials. Ensure that the diameter of the milling cutter is approximately 50% of the slot width, providing sufficient movement space for the milling cutter, and ensuring that the cutting angle does not increase or generate excessive cutting heat.
The optimal tool for a specific machining process depends not only on the material being cut, but also on the cutting type and milling method used. By optimizing cutting tools, cutting speed, feed rate, and machining programming skills, components can be produced faster and better at lower processing costs.


