


How many common surface treatment methods do you know?
Surface treatment is a process method of artificially forming a surface layer on the surface of a substrate material that has different mechanical, physical, and chemical properties from the substrate. The purpose of surface treatment is to meet the requirements of corrosion resistance, wear resistance, decoration, or other special functions of the product. Today, we will share some common surface treatment methods and see how many you know~
1, Polishing
Polishing refers to the process of using mechanical, chemical, or electrochemical forces to reduce the surface roughness of a workpiece, in order to obtain a bright and flat surface. It is the process of modifying the surface of a workpiece using polishing tools and abrasive particles or other polishing media. Polishing cannot improve the dimensional or geometric accuracy of the workpiece, but rather aims to obtain a smooth surface or mirror gloss, sometimes also used to eliminate gloss (extinction). Usually, polishing wheels are used as polishing tools. Polishing wheels are generally made by stacking multiple layers of canvas, felt, or leather, with metal circular plates clamped on both sides. The rim of the wheel is coated with a polishing agent uniformly mixed with micro abrasive and grease. During polishing, the high-speed rotating polishing wheel (with a circumferential speed of over 20 meters/second) presses against the workpiece, causing the abrasive to roll and cut slightly on the surface of the workpiece, thereby obtaining a bright machining surface. The surface roughness can generally reach Ra0.63-0.01 micrometers; When using non greasy matte polishing agents, the bright surface can be matted to improve appearance. For different polishing processes: rough polishing (basic polishing process), intermediate polishing (precision machining process), and precision polishing (polishing process), selecting appropriate polishing wheels can achieve the best polishing effect and improve polishing efficiency.
2, Sandblasting
The process of cleaning and roughening the substrate surface by utilizing the impact of high-speed sand flow. Using compressed air as the power, a high-speed jet beam is formed to spray materials (copper ore sand, quartz sand, diamond sand, iron sand, Hainan sand) at high speed onto the surface of the workpiece to be treated, causing changes in the appearance or shape of the outer surface of the workpiece. Due to the impact and cutting effects of abrasives on the workpiece surface, the workpiece surface obtains a certain degree of cleanliness and different roughness, improving the mechanical properties of the workpiece surface, Therefore, the fatigue resistance of the workpiece is improved, the adhesion between it and the coating is increased, the durability of the coating is extended, and it is also beneficial for the leveling and decoration of the coating.

III wire drawing
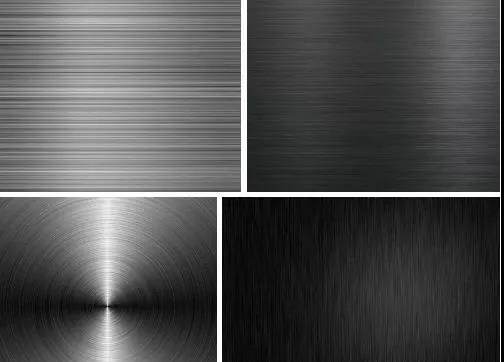
It is a surface treatment method that forms lines on the surface of workpieces by grinding products to achieve decorative effects. According to the different patterns after drawing, it can be divided into: straight drawing, irregular drawing, ripple, and spiral drawing. Surface wire drawing treatment is a surface treatment method that forms lines on the surface of workpieces by grinding products to achieve decorative effects. Due to its ability to reflect the texture of metal materials, surface wire drawing treatment has gained increasing popularity and widespread application among users.
4, Anodization
An electrolytic oxidation process in which the surface of aluminum and aluminum alloys is typically transformed into a layer of oxide film, which has protective, decorative, and other functional properties. Starting from this definition, anodizing of aluminum only includes the process of generating an anodized film. Using metal or alloy components as anodes, an oxide film is formed on their surface by electrolysis. Metal oxide films change the surface state and properties, such as surface coloring, improving corrosion resistance, enhancing wear resistance and hardness, and protecting the metal surface. For example, aluminum anodizing involves placing aluminum and its alloys in corresponding electrolytes (such as sulfuric acid, chromic acid, oxalic acid, etc.) as anodes, and conducting electrolysis under specific conditions and external current. Anodized aluminum or its alloys are oxidized, forming a thin layer of aluminum oxide on the surface, with a thickness of 5-30 microns. The hard anodized oxide film can reach 25-150 microns. Anodized aluminum or its alloys improve their hardness and wear resistance, reaching 250-500 kilograms per square millimeter. They have good heat resistance, a high melting point of 2320K for hard anodized oxide films, excellent insulation properties, and a breakdown voltage resistance of up to 2000V, enhancing their corrosion resistance ω= 0.03 NaCl salt spray does not corrode for thousands of hours. The thin oxide film contains a large number of micropores, which can adsorb various lubricants and are suitable for manufacturing engine cylinders or other wear-resistant parts; The membrane micropores have strong adsorption capacity and can be colored into various beautiful and vibrant colors. Non ferrous metals or their alloys (such as aluminum, magnesium, and their alloys) can undergo anodizing treatment, which is widely used in mechanical parts, aircraft and automotive components, precision instruments and radio equipment, daily necessities, and building decoration. Generally speaking, the anode is made of aluminum or aluminum alloy, while the cathode is made of lead plate. The aluminum and lead plates are placed together in an aqueous solution, which contains sulfuric acid, oxalic acid, chromic acid, etc., for electrolysis to form an oxide film on the surface of the aluminum and lead plates. Among these acids, the most widespread is anodic oxidation using sulfuric acid.
process flow
Monochrome and gradient colors: polishing/sandblasting/drawing → degreasing → anodizing → neutralization → dyeing → sealing → drying
Dual color: ① Polishing/sandblasting/drawing → degreasing → shielding → anodizing 1 → anodizing 2 → sealing → drying
② Polishing/sandblasting/drawing → degreasing → anodizing 1 → laser engraving → anodizing 2 → sealing → drying
Technical characteristics
1. Enhance strength,
2. Implement any color except white.
3. Realize nickel free sealing to meet the nickel free requirements of countries such as Europe and the United States.
5, Electrophoresis
The process is divided into anodic electrophoresis and cathodic electrophoresis. If the coating particles are negatively charged and the workpiece is an anode, the coating particles will deposit a film on the workpiece under the action of electric field force, which is called anodic electrophoresis; On the contrary, if the coating particles are positively charged and the workpiece is the cathode, the deposition of coating particles on the workpiece is called cathodic electrophoresis.
The general process flow of anodic electrophoresis is as follows: pre-treatment of the workpiece (degreasing → hot water washing → rust removal → cold water washing → phosphating → hot water washing → passivation) → anodic electrophoresis → post-treatment of the workpiece (clean water washing → drying).
1. Remove oil. The solution is generally a hot alkaline chemical degreasing solution, with a temperature of 60 ℃ (steam heating) and a time of about 20 minutes.
2. Hot water washing. Temperature 60 ℃ (steam heating), time 2 minutes.
3. Rust removal. Using H2SO4 or HCl, such as hydrochloric acid rust removal solution, the total acidity of HCl should be ≥ 43 points; Free acidity>41 points; Add 1.5% cleaning agent; Wash at room temperature for 10-20 minutes.
4. Wash with cold water. Wash with flowing cold water for 1 minute.
5. Phosphatization. Using medium temperature phosphating (phosphating at 60 ℃ for 10 minutes), the phosphating solution can be used as a commercially available finished product.
The above process can also be replaced by sandblasting → water washing.
6. Passivation. Use drugs that are compatible with the phosphating solution (provided by the manufacturer selling the phosphating solution) and let it sit at room temperature for 1-2 minutes.
7. Anodic electrophoresis. Electrolyte composition: H08-1 black electrophoretic paint, solid content mass fraction 9% -12%, distilled water mass fraction 88% -91%. Voltage: (70 ± 10) V; Time: 2-2.5 minutes; Paint temperature: 15-35 ℃; Paint solution pH value: 8-8.5. Be sure to turn off the power when the workpiece enters or exits the groove. During the electrophoresis process, the current gradually decreases as the paint film thickens.
8. Wash with clean water. Wash in flowing cold water.
9. Drying. Bake in an oven at a temperature of (165 ± 5) ℃ for 40-60 minutes.

VI PVD
PVD is the abbreviation for Physical Vapor Deposition, which refers to the use of low voltage and high current arc discharge technology under vacuum conditions. Gas discharge is used to evaporate the target material and ionize both the evaporated substance and gas. The acceleration effect of the electric field is used to deposit the evaporated substance and its reaction products on the workpiece. The physical vapor deposition technology has a simple process, improves the environment, is pollution-free, consumes less materials, forms a uniform and dense film, and has strong adhesion to the substrate. This technology is widely used in aerospace, electronics, optics, machinery, construction, light industry, metallurgy, materials and other fields. It can prepare film layers with characteristics such as wear resistance, corrosion resistance, decoration, conductivity, insulation, photoconductivity, piezoelectricity, magnetism, lubrication, superconductivity, etc.
7, Electroplating
Electroplating is the process of plating a thin layer of other metals or alloys on certain metal surfaces using the principle of electrolysis. It is a process that uses electrolysis to attach a metal film to the surface of metal or other material components, thereby preventing metal oxidation (such as rust), improving wear resistance, conductivity, reflectivity, corrosion resistance (such as copper sulfate), and enhancing aesthetics. The outer layer of many coins is also electroplated.
8, Etching
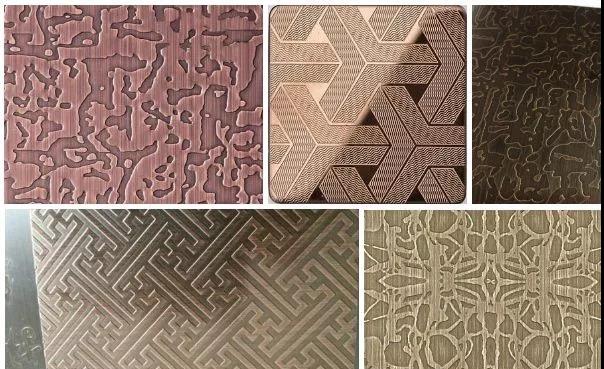
The commonly referred to etching, also known as photochemical etching, refers to the removal of the protective film on the area to be etched after exposure plate making and development, and the contact with chemical solution during etching to achieve the effect of dissolution corrosion, forming a concave convex or hollow forming effect.
Process flow:
Exposure method: According to the graphics, the engineering will determine the size of the material preparation, material preparation, material cleaning, drying, film application or coating, drying, exposure, development, drying, etching, film removal, and OK
Screen printing method: cutting → cleaning the plate (stainless steel and other metal materials) → screen printing → etching → delamination → OK
9, Spray coating
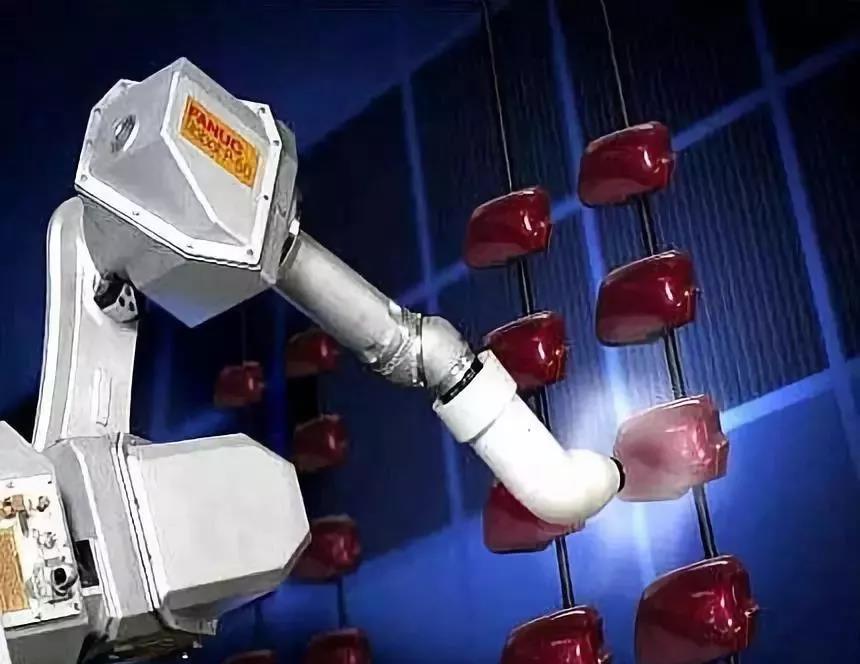
Spray coating is a coating method that uses a spray gun or disc atomizer, with the help of pressure or centrifugal force, to disperse into uniform and fine droplets, and apply them to the surface of the coated object. It can be divided into air spraying, airless spraying, electrostatic spraying, and various derivative methods of the basic spraying forms mentioned above, such as high flow low pressure atomization spraying, thermal spraying, automatic spraying, multi group spraying, etc. The spraying operation has high production efficiency and is suitable for manual operation and industrial automation production. It is widely used in hardware, plastics, furniture, military industry, ships and other fields. It is the most common coating method nowadays; The spraying operation requires a dust-free workshop with environmental requirements ranging from one million to one hundred levels. The spraying equipment includes a spray gun, spray painting room, paint supply room, curing furnace/drying furnace, spraying workpiece conveying equipment, defogging and wastewater treatment equipment, and exhaust gas treatment equipment. High flow and low pressure atomization spraying results in low atomization pressure and low air jet velocity. The low atomization coating operating speed improves the situation where the coating rebounds from the surface of the coated object. The painting rate has been increased from 30% to 40% of ordinary air spraying to 65% to 85%. Spray the coating onto the leather surface using a spray gun or spray machine in light leather finishing.
10, Laser carving
Also known as laser engraving or laser marking, it is a surface treatment process that uses optical principles.
Using a high-intensity focused laser beam emitted by a laser at the focal point The effect of marking is to expose deep substances through the evaporation of surface substances, or to cause chemical and physical changes in surface substances through light energy, or to burn off some substances through light energy and "engrave" them, or to burn off some substances through light energy and display the desired etched graphics and text.


